Procuring medical-grade packaging involves a complex balance between material integrity, regulatory compliance, and budget management. For laboratory and veterinary professionals, the focus often shifts from a simple search for the lowest medicine bottle price to a comprehensive evaluation of total cost of ownership, including the risks of contamination or product degradation.
The shift toward high-performance polymers like Polypropylene (PP) and Polyethylene (PE) has redefined the stability of liquid medicines. Unlike traditional glass, these materials offer shatter-resistance and lighter weights, which significantly reduce logistics costs and workplace hazards in high-volume clinical environments.
This analysis explores the technical drivers of pricing in pharmaceutical packaging, the critical role of UV protection in vaccine stability, and the operational frameworks used to select the most reliable containment systems for veterinary and laboratory use.


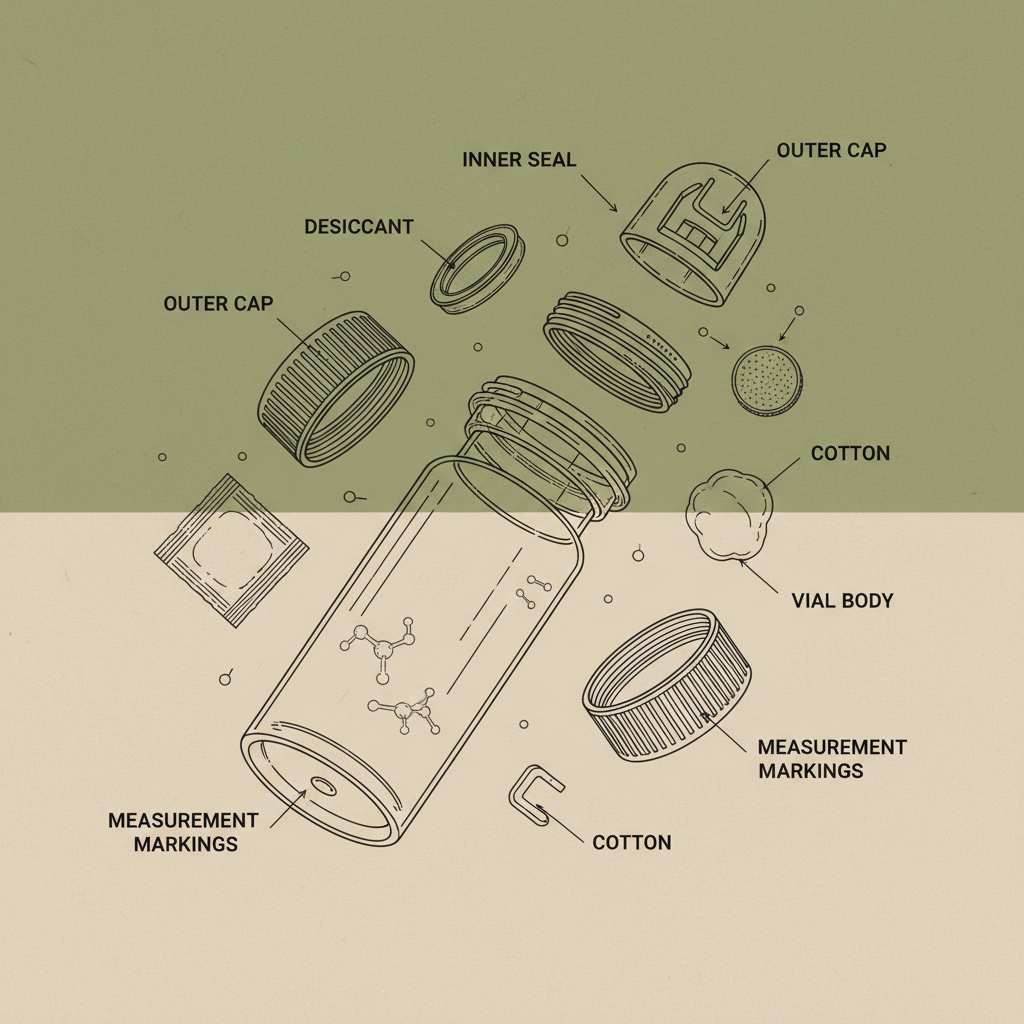
Modern pharmaceutical packaging relies on the "Injection and Blowing" process to ensure wall uniformity and structural stability. This method allows for a seamless bottle body, which is essential for maintaining a vacuum or pressure seal, especially in vaccine vials ranging from 10ml to 500ml.
Sterility is achieved through rigorous purification workshop standards and the application of ethylene oxide (EO) gas sterilization. This ensures that containers are free from microbial contaminants before they ever reach the filling line, a non-negotiable requirement for injectable medicines.
The selection between Polyethylene (PE) and Polypropylene (PP) is driven by the thermal and chemical requirements of the stored liquid. PP is typically preferred for applications requiring high-temperature resistance and pressure stability, such as those undergoing autoclave sterilization, while PE offers excellent chemical inertness for a wide range of reagents.
Sealing mechanisms further define the container's integrity. The combination of rubber plugs and aluminum caps creates a robust barrier that prevents leakage during transportation. This is particularly critical for veterinary medicines transported over long distances to rural clinics, where temperature fluctuations and physical shocks are common.
Beyond the material, the ergonomic design of the vial—including the neck finish and body grip—facilitates accurate dosing and reduces the risk of accidental spills in fast-paced laboratory settings. The smooth exterior also ensures that labeling remains legible, aiding in the traceability of batch numbers and expiration dates.
Many liquid medicines and vaccines are photo-sensitive, meaning exposure to ultraviolet (UV) light can catalyze chemical reactions that degrade the potency of the active pharmaceutical ingredient (API). To counteract this, brown translucent plastic is utilized as a protective barrier.
The use of amber-tinted medical polymers does not merely change the appearance of the vial; it creates a specific spectral filter that blocks harmful UV wavelengths while allowing visual inspection of the liquid level.
This balance between protection and visibility is essential for safety. It prevents the wastage of expensive medicines by ensuring stability during extended storage and enables clinicians to verify volume before administration, reducing dosing errors in veterinary practices.
When analyzing the medicine bottle price, buyers must look beyond the unit cost. The pricing is fundamentally influenced by the level of sterilization required, the grade of the polymer (medical vs. industrial), and the complexity of the sealing system (e.g., tamper-evident lids).
Furthermore, the production volume and the specific specifications—such as the precision of the wall thickness—impact the final cost. High-precision bottles produced in clean rooms naturally command a premium due to the operational overhead of maintaining ISO and FDA-certified environments.
In a typical industrial veterinary setting, the priority is the transition from cold chain storage to field administration. Shatter-resistant plastic vials are indispensable here, as they eliminate the risk of glass shards contaminating a vaccination site or causing injuries to personnel during mobile operations.
For laboratory research, the focus shifts to chemical compatibility. When storing reagents or liquid vaccines, the inert nature of PP and PE prevents leaching and adsorption, ensuring that the concentration of the medicine remains precise for experimental validity.
The industry is moving toward increased customization of bottle geometry to fit automated filling lines more efficiently. This reduces the waste of expensive medicinal liquids and increases the throughput of pharmaceutical plants.
Another significant trend is the adoption of more advanced tamper-evident closures. As global supply chains for veterinary medicines grow, the need to guarantee that a vial has not been compromised during transit has become a primary requirement for procurement officers.
Sustainability is also entering the conversation, with a push toward medical-grade polymers that maintain sterility and safety while reducing the overall carbon footprint of the manufacturing process, particularly in the injection-blowing phase.
Choosing the right container requires a trade-off analysis between material properties and application needs. While glass offers absolute gas impermeability, plastic provides durability and cost-efficiency that is often more practical for large-scale livestock vaccination programs.
Decision-makers should evaluate the specific UV sensitivity of their product and the temperature extremes of their logistics chain. A vial that is cost-effective in a controlled lab may fail in a field environment if it lacks the necessary impact resistance or sealing quality.
Ultimately, the value of the packaging is measured by the stability of the medicine it protects. Investing in higher-specification containers can prevent the catastrophic loss of entire vaccine batches, making "cheap" packaging the most expensive option in the long run.
| Evaluation Factor | Polypropylene (PP) | Polyethylene (PE) | Borosilicate Glass |
|---|---|---|---|
| Thermal Resistance | High (Autoclavable) | Moderate | Very High |
| Impact Durability | Very High | High | Low (Fragile) |
| UV Protection | Possible (Amber) | Possible (Amber) | Possible (Amber) |
| Chemical Inertness | High | Very High | Highest |
| Transport Weight | Low | Low | High |
| Risk of Leaks | Low (with Al cap) | Low (with Al cap) | Moderate (Breakage) |
The price is primarily driven by the grade of the raw polymer (medical-grade PP vs. PE), the sterilization method used (such as ethylene oxide gas), and the environment in which it is produced (100,000-grade clean rooms). Additionally, the complexity of the closure system, such as combining rubber plugs with aluminum caps for airtight sealing, adds to the cost but ensures the safety and stability of the medicine during transport.
Many active pharmaceutical ingredients in vaccines are photo-sensitive and can degrade when exposed to UV light. Brown or amber-tinted plastic acts as a spectral filter, blocking harmful ultraviolet rays while still allowing clinicians to visually inspect the liquid level. This ensures the potency of the vaccine is maintained over extended storage periods and during transit.
The injection-blowing process allows for the creation of a bottle in a single operational sequence, which results in a more uniform bottle wall and a smoother exterior. This consistency is vital for pharmaceutical applications because it ensures that the internal volume is precise and that there are no structural weak points that could lead to leaks or contamination under pressure.
Yes, medical-grade plastic bottles can be sterilized using ethylene oxide (EO) gas in specialized purification workshops. This process ensures the containers are sterile and clean without subjecting the plastic to extreme heat that might warp the structure. When paired with sterile rubber plugs and aluminum seals, these bottles are suitable for the safe administration of injectable veterinary and human medicines.
The primary advantage is shatter-resistance. In field operations, where vials are transported in mobile units and handled in uncontrolled environments, glass poses a significant risk of breakage, leading to product loss and safety hazards. Plastic vials (PP/PE) are lightweight and durable, ensuring that the vaccine remains intact even if the container is dropped, which is critical for large-scale livestock vaccination programs.
Buyers should verify the supplier's production qualifications, specifically looking for ISO 9001 and FDA certifications. It is important to confirm the existence of certified clean rooms (e.g., 100,000-grade) and a validated sterilization process. A capable supplier should also offer a wide range of specifications (e.g., 10-500ml) and demonstrate the ability to provide consistent wall thickness and sealing integrity across large batches.
The procurement of pharmaceutical packaging is a critical link in the medical supply chain. By prioritizing material science—specifically the use of UV-blocking polymers and sterile production processes—providers can ensure that life-saving vaccines and medicines maintain their efficacy from the factory to the animal.
While the initial medicine bottle price may vary, the true value lies in the reduction of risk. Transitioning to high-quality, shatter-resistant plastic packaging not only enhances operational safety in the field but also provides a reliable foundation for modern veterinary and laboratory healthcare practices.