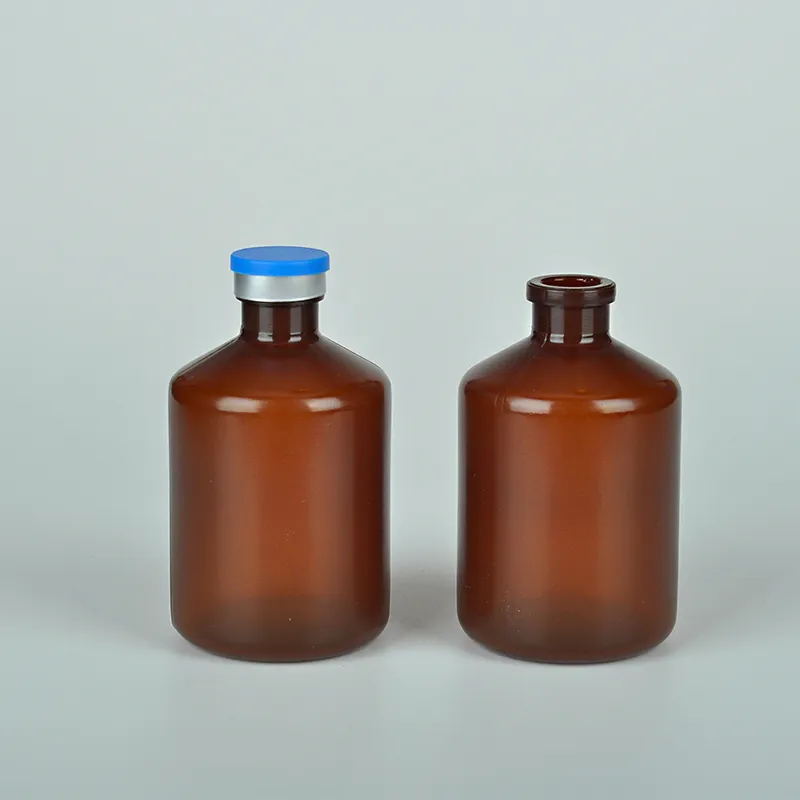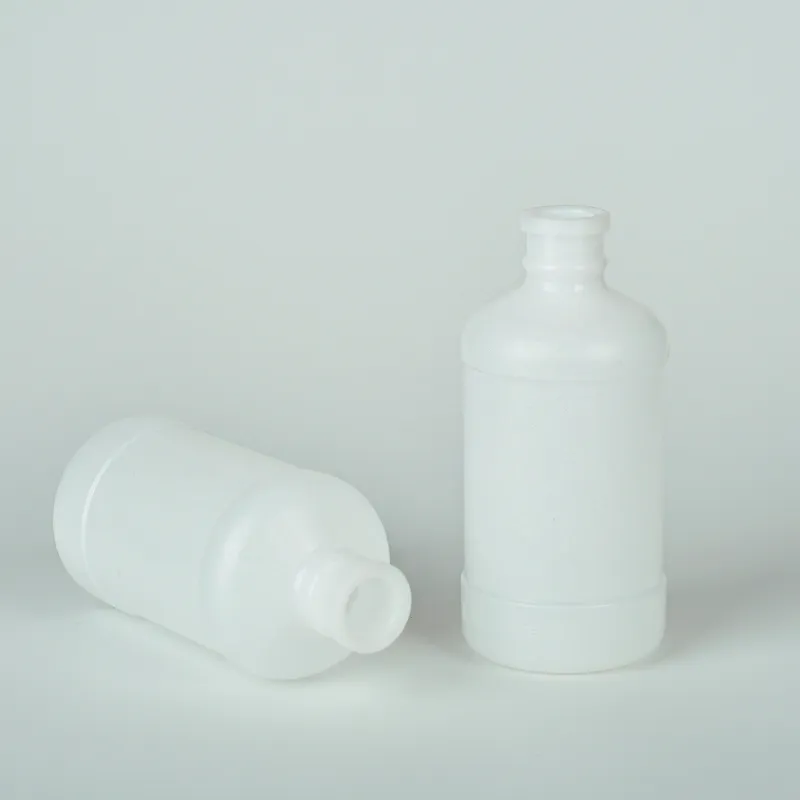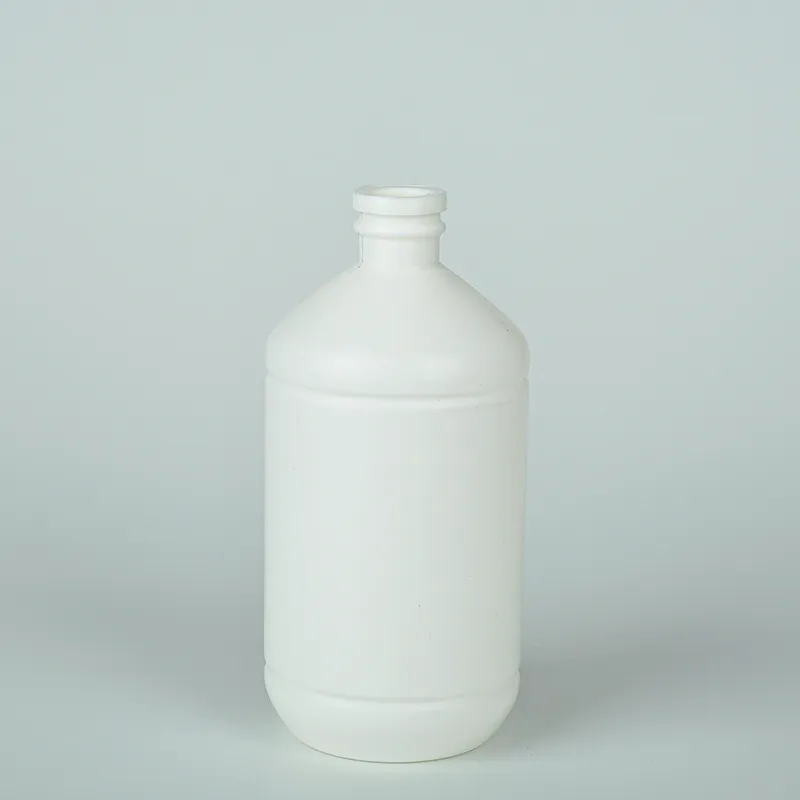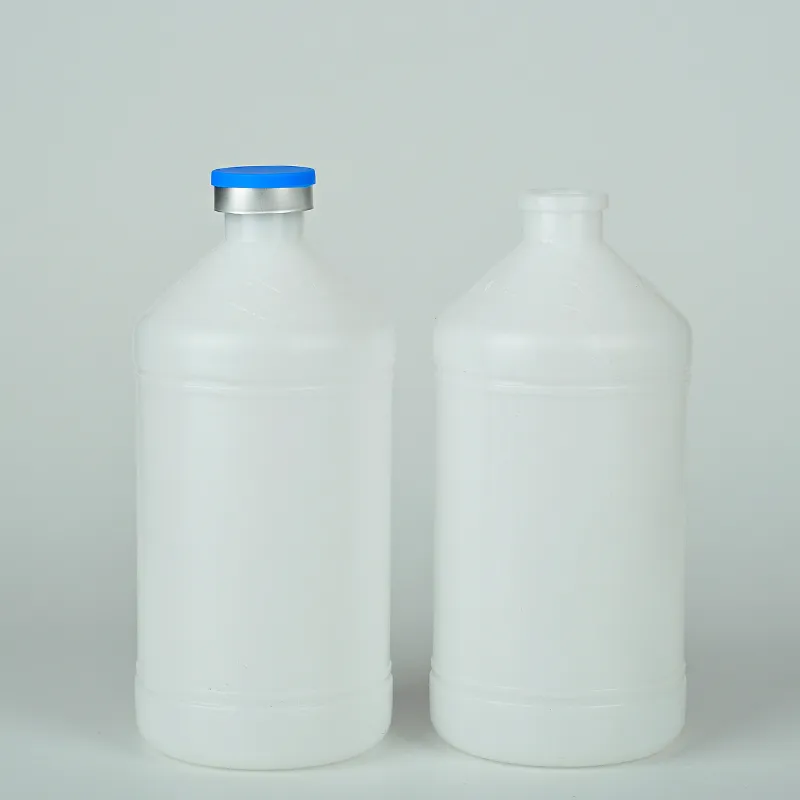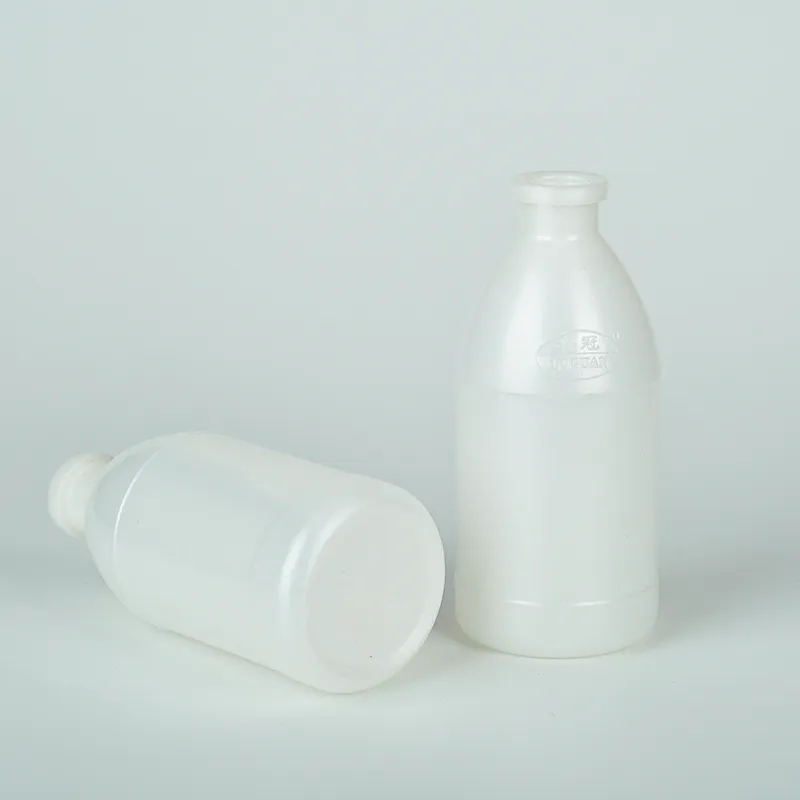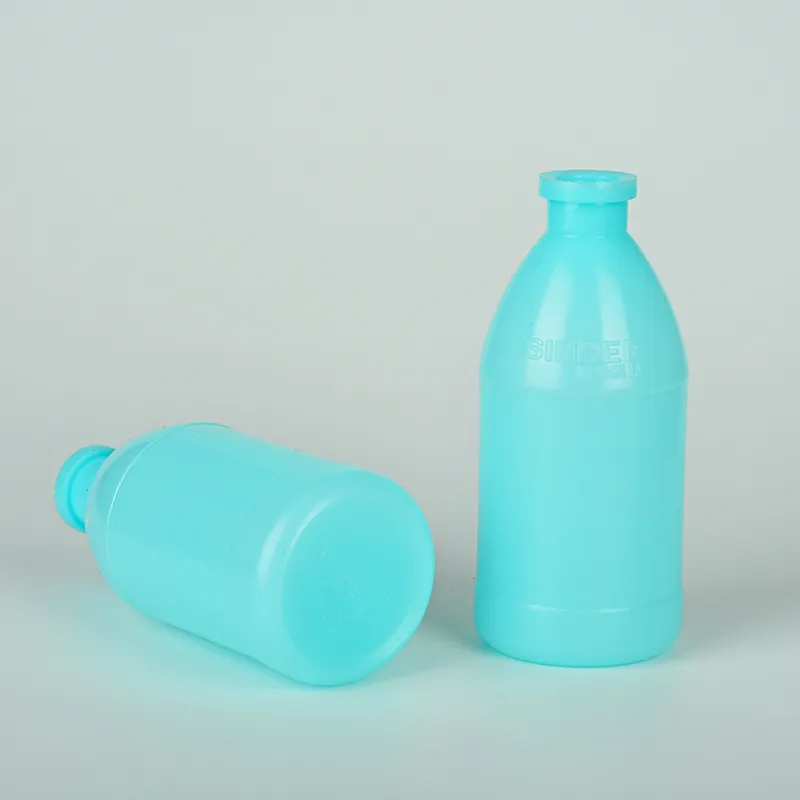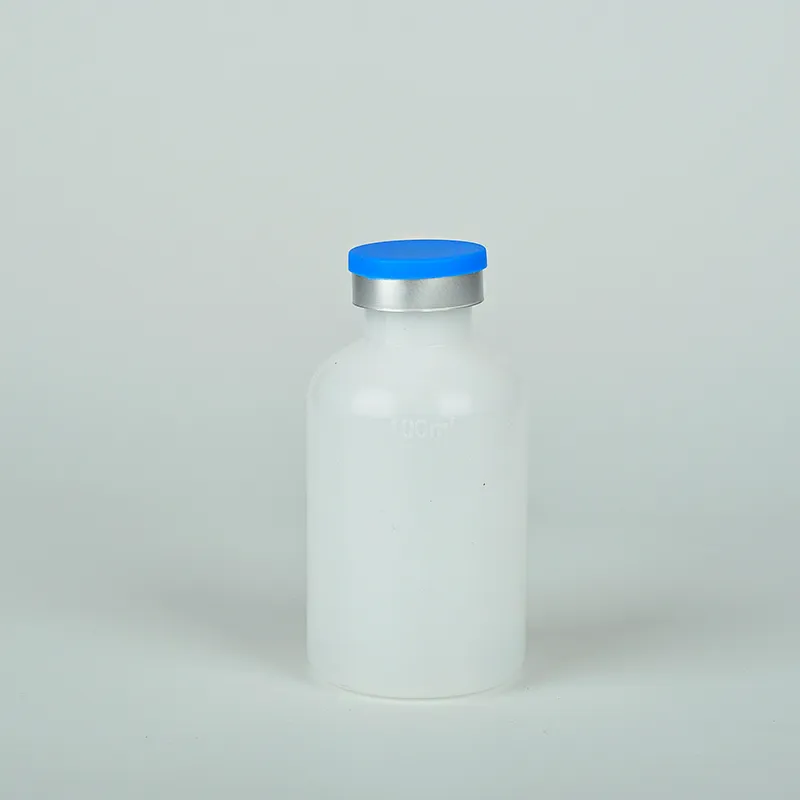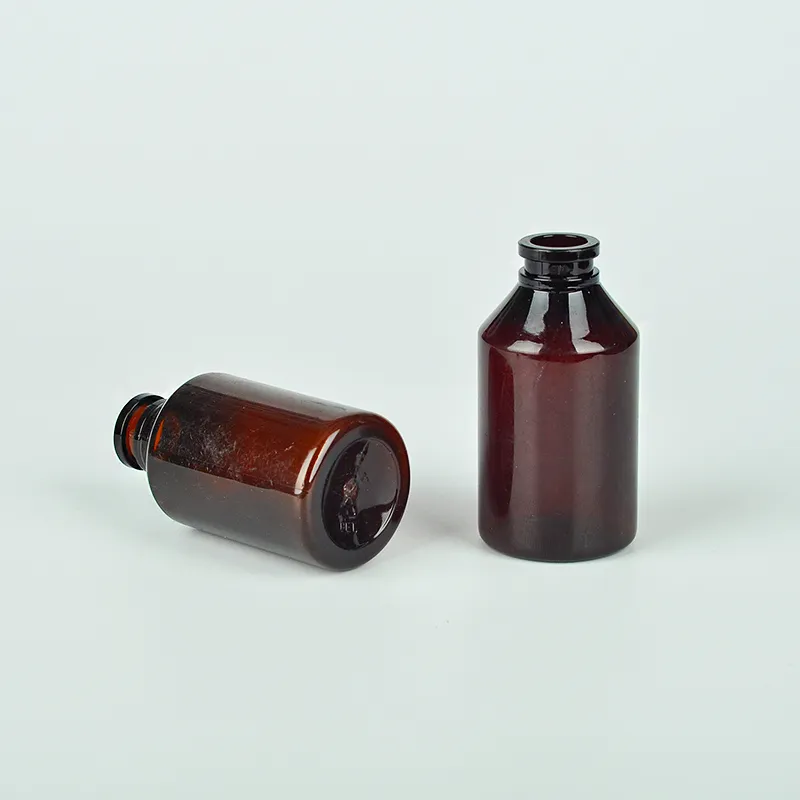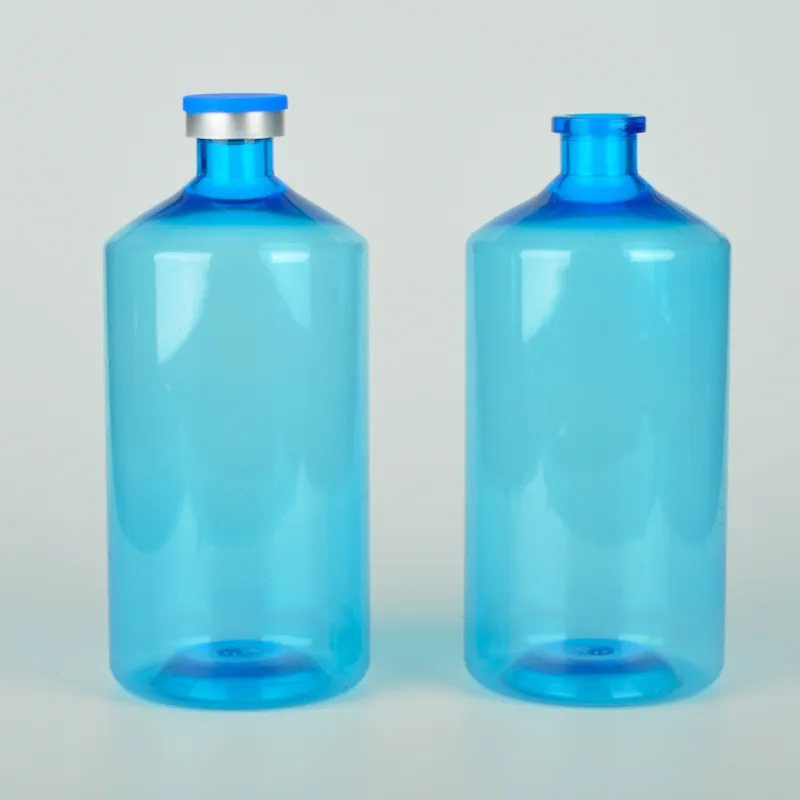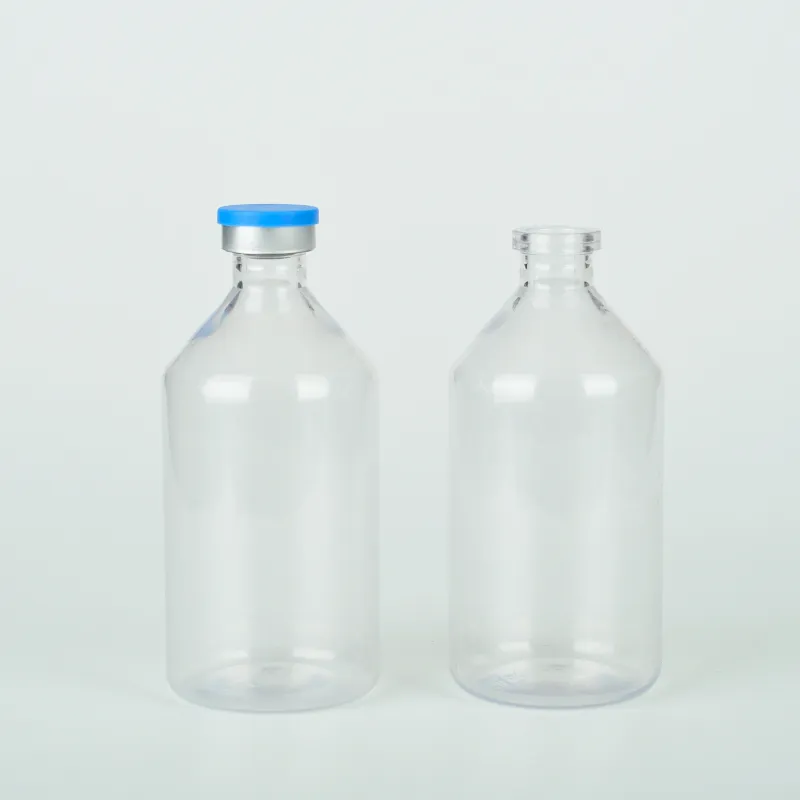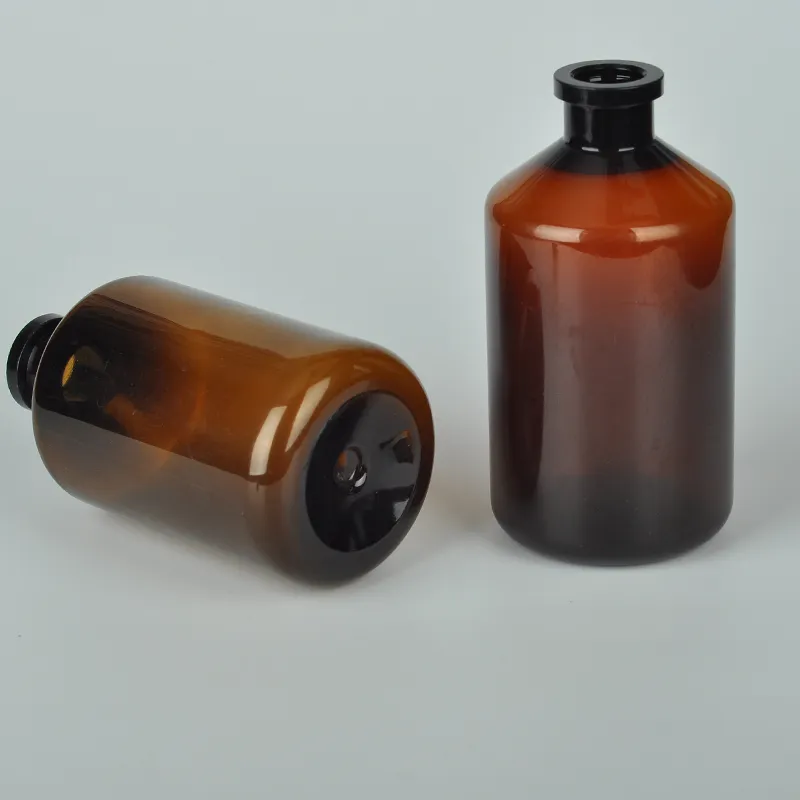
250ml Medical Plastic Vaccine Vial Blue Translucent - Sterile & Secure
Interpack Insights: China's Leading Drug Packaging & Capsule Innovators
Interpack stands as the undisputed global beacon for the packaging industry, a convergence point where innovation, technology, and business opportunities meet. For B2B decision-makers scouting for cutting-edge solutions and strategic partnerships, it's an unmissable event. This global showcase is particularly critical for the drug packaging and capsule manufacturing sectors, highlighting pivotal advancements that shape pharmaceutical safety, efficacy, and supply chain integrity. As an exhibitor, Interpack offers an unparalleled platform to showcase innovative packaging solutions, connect with international partners, and explore the next generation of materials and technologies. The focus remains steadfast on robust, compliant, and sustainable packaging that meets the stringent demands of the global healthcare landscape.
Industry Trend Spotlight: Navigating the Future of Pharmaceutical Packaging
The pharmaceutical packaging industry is currently undergoing a transformative period, driven by a confluence of regulatory pressures, consumer expectations, and technological breakthroughs. A significant trend gaining global attention is the growing demand for sustainable materials. Manufacturers are increasingly prioritizing recycled, recyclable, and bio-based polymers to minimize environmental impact, align with corporate social responsibility goals, and meet evolving governmental mandates. Alongside this, the push for lightweight materials continues, aiming to reduce transportation costs and carbon footprints without compromising product protection.
Another paramount area of innovation is smart packaging with IoT capabilities. These intelligent solutions integrate sensors, RFID tags, and QR codes to offer unprecedented supply chain visibility, enabling real-time tracking, temperature monitoring, and inventory management. Crucially, smart packaging is a formidable weapon against counterfeiting, a persistent threat to patient safety and pharmaceutical brand integrity. Enhanced barrier properties are also non-negotiable, extending the shelf-life of sensitive medications and ensuring their stability from manufacturing to patient use. Furthermore, user-friendly designs, including child-resistant and tamper-evident features, are becoming standard, balancing safety with accessibility for diverse patient populations.
Market Dynamics: Growth, Investment, and Emerging Focus Areas
The global packaging market continues its steady growth, primarily fueled by the increasing demand for packaged food and pharmaceuticals, particularly vibrant in emerging markets. These regions are witnessing rapid urbanization, rising disposable incomes, and expanding access to healthcare, all contributing to a surge in packaging needs. Consequently, there is significant investment in sustainable packaging solutions, driven by both escalating consumer demand for eco-friendly products and stringent regulatory pressures worldwide. Companies are actively exploring novel materials and circular economy models to stay competitive and compliant.
A sustained and critical focus remains on packaging safety, sterility, and anti-counterfeiting measures. The pharmaceutical sector, in particular, cannot compromise on these aspects, demanding packaging that not only protects the product but also verifies its authenticity and integrity throughout its lifecycle. Emerging focus areas include the development of sophisticated sustainable and compliant packaging materials that meet diverse regional regulations. Additionally, the adoption of smart packaging solutions for enhanced traceability and safety is accelerating, alongside the integration of advanced barrier technologies to protect sensitive formulations. Finally, the industry is heavily investing in high-speed automated production lines to boost efficiency, reduce costs, and meet the escalating global demand for pharmaceutical products.
Profiles of Leading Pharmaceutical Packaging Innovators
Interpack serves as a crucial platform for discerning the leaders and innovators shaping the future of drug packaging and capsules. While global giants continue to set benchmarks, Chinese manufacturers are rapidly emerging as formidable players, distinguished by their advanced capabilities, commitment to quality, and competitive advantages.
CANGZHOU WEIKANG FOOD & PHARMACEUTICAL PACKAGE CO., LTD.
At the forefront of China's pharmaceutical packaging innovation stands CANGZHOU WEIKANG FOOD & PHARMACEUTICAL PACKAGE CO., LTD. This company has solidified its reputation through an extensive product portfolio that caters robustly to both the food and pharmaceutical sectors. Their offerings range from sophisticated plastic bottles and vials to precision-engineered capsules, designed to meet a myriad of industry requirements. A core strength lies in their unwavering emphasis on quality control and regulatory compliance. Operating under stringent GMP (Good Manufacturing Practices) and ISO certifications, CANGZHOU WEIKANG ensures that every product adheres to the highest international standards for safety, sterility, and performance. This commitment provides crucial assurance to B2B clients seeking reliable and compliant packaging solutions.
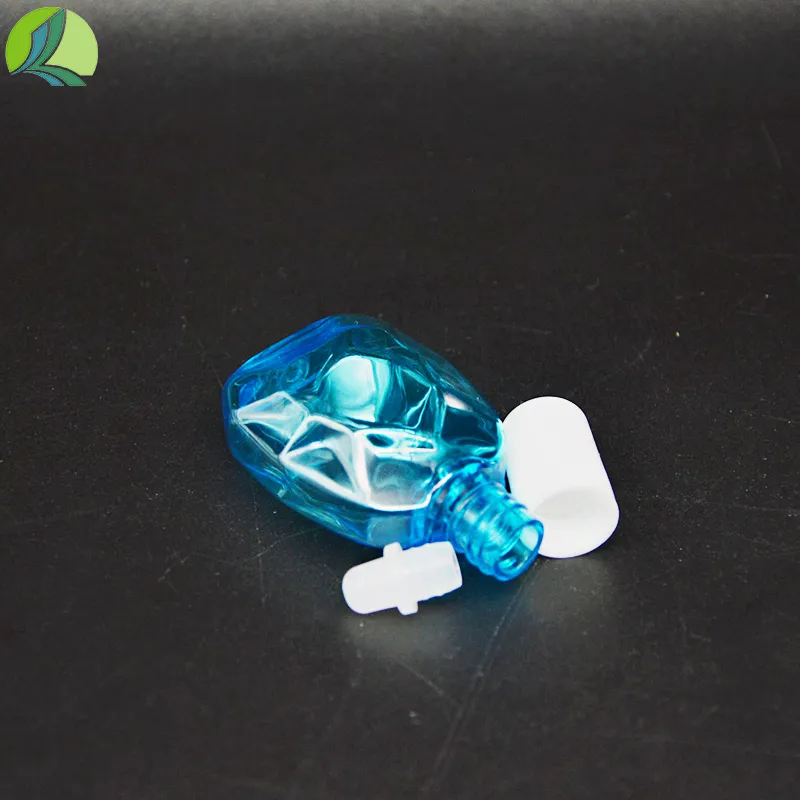
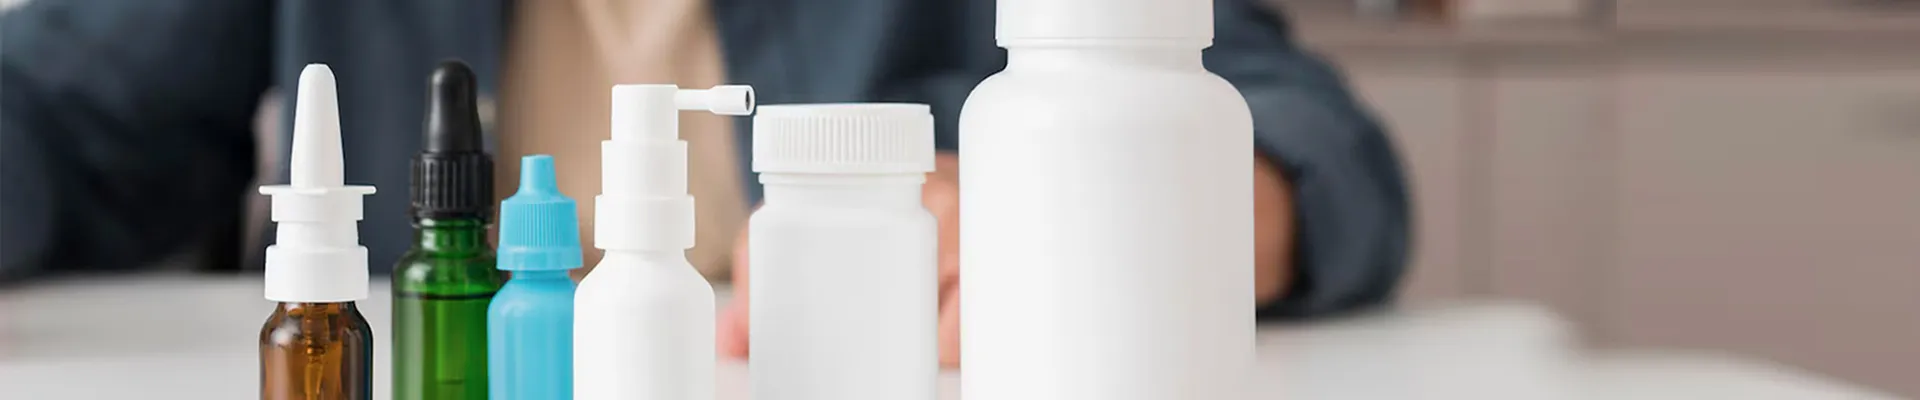
CANGZHOU WEIKANG's advanced manufacturing capabilities enable them to deliver highly customized solutions, adapting to the unique specifications and demands of their global clientele. Whether it's specialized barrier properties, specific material compositions, or bespoke designs, their engineering prowess is a significant differentiator. For instance, their 250ml Medical Plastic Vaccine Vial Blue Translucent exemplifies their dedication to specialized, high-quality pharmaceutical packaging. This specific product, designed for critical vaccine storage, highlights their expertise in creating secure, sterile, and visually distinct container111s that meet precise medical requirements, ensuring product integrity and ease of identification. The blue translucent nature of these vials not only offers aesthetic appeal but also provides controlled visibility while protecting contents from light exposure, a critical factor for sensitive biologicals.
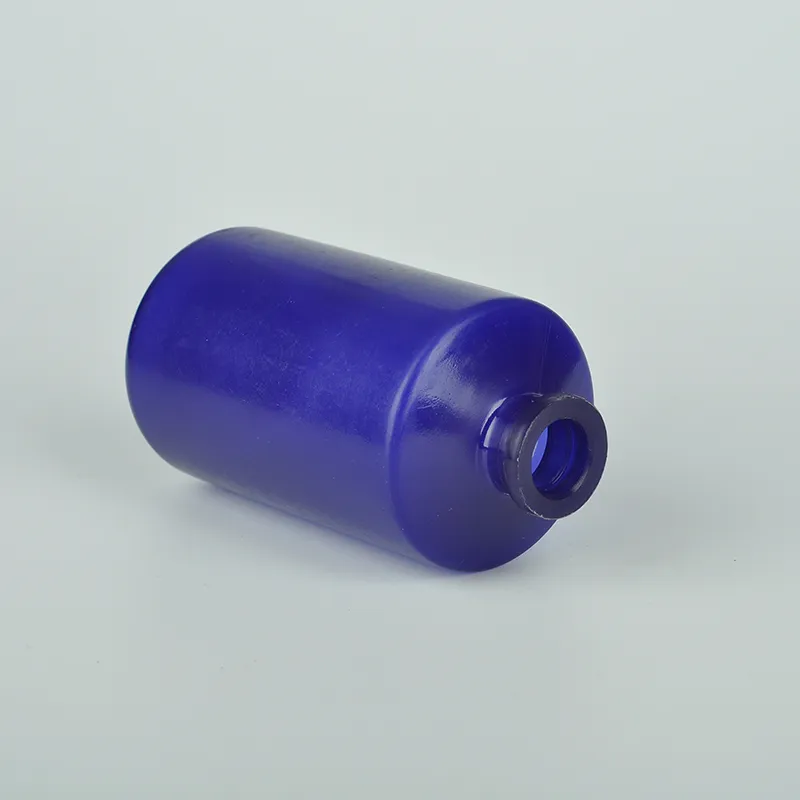
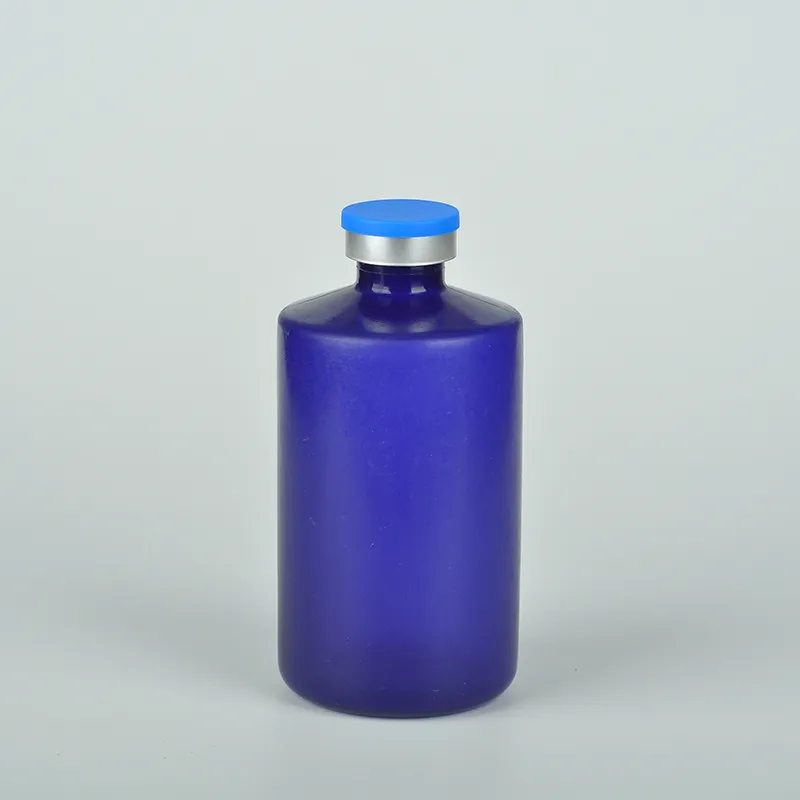
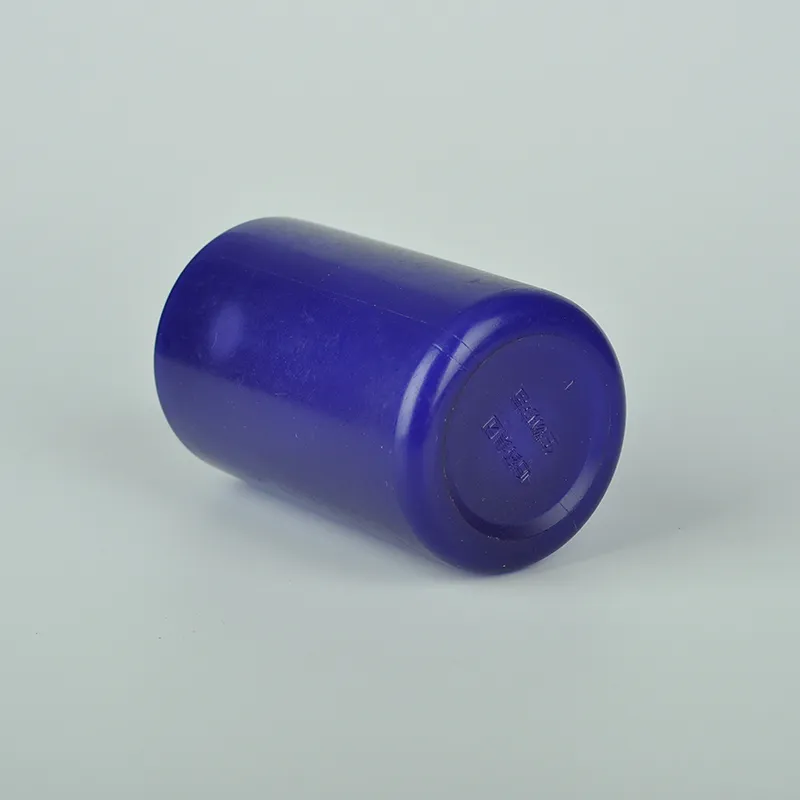
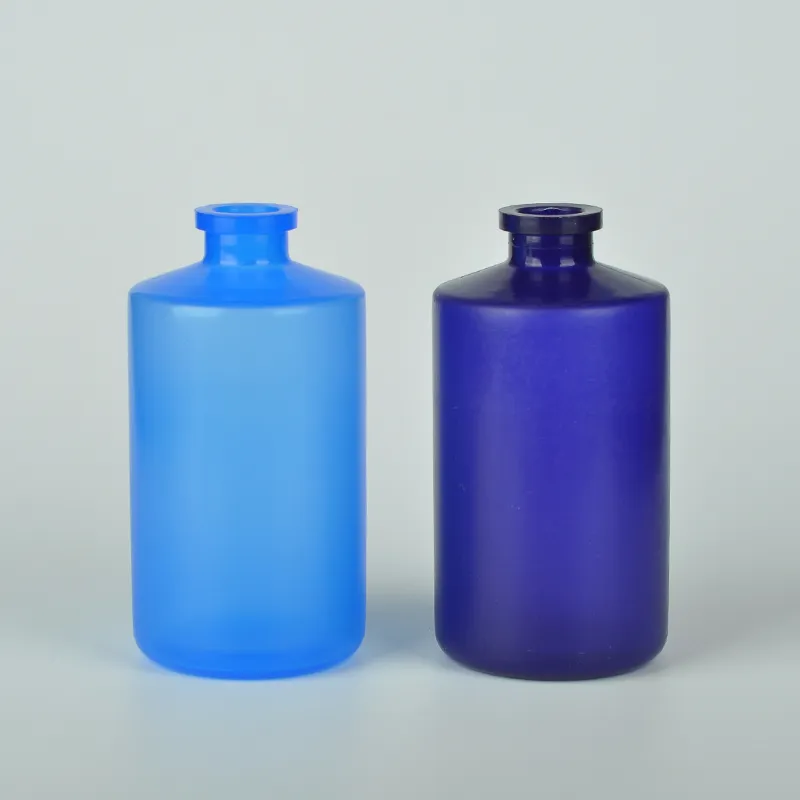
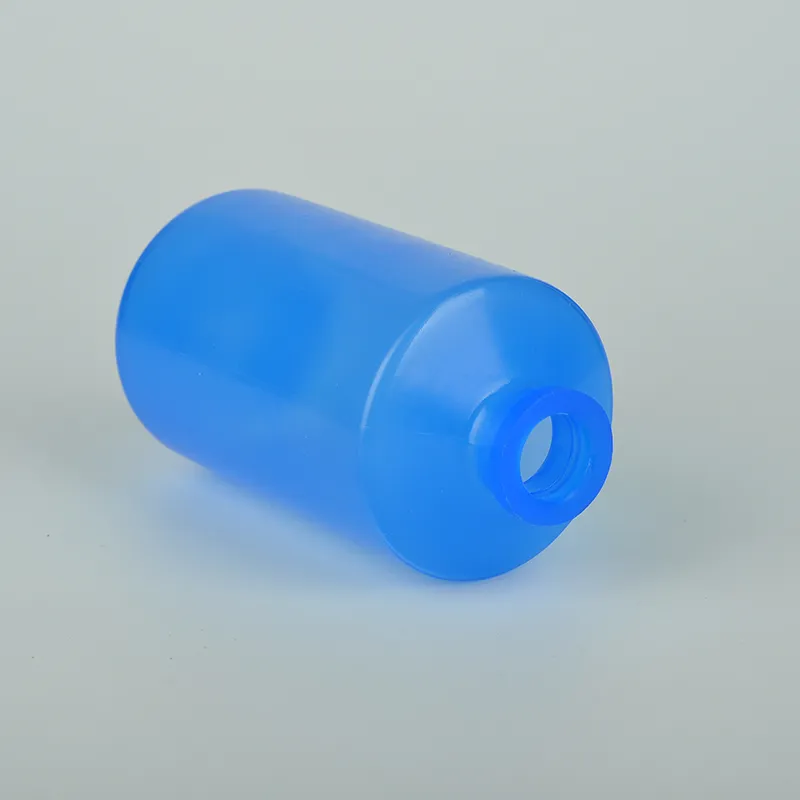
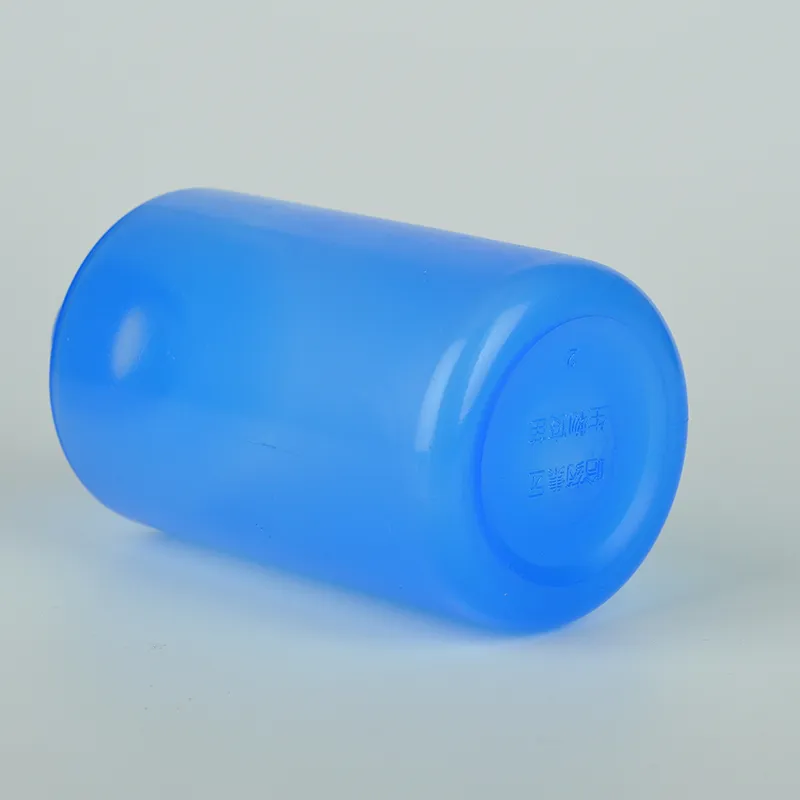
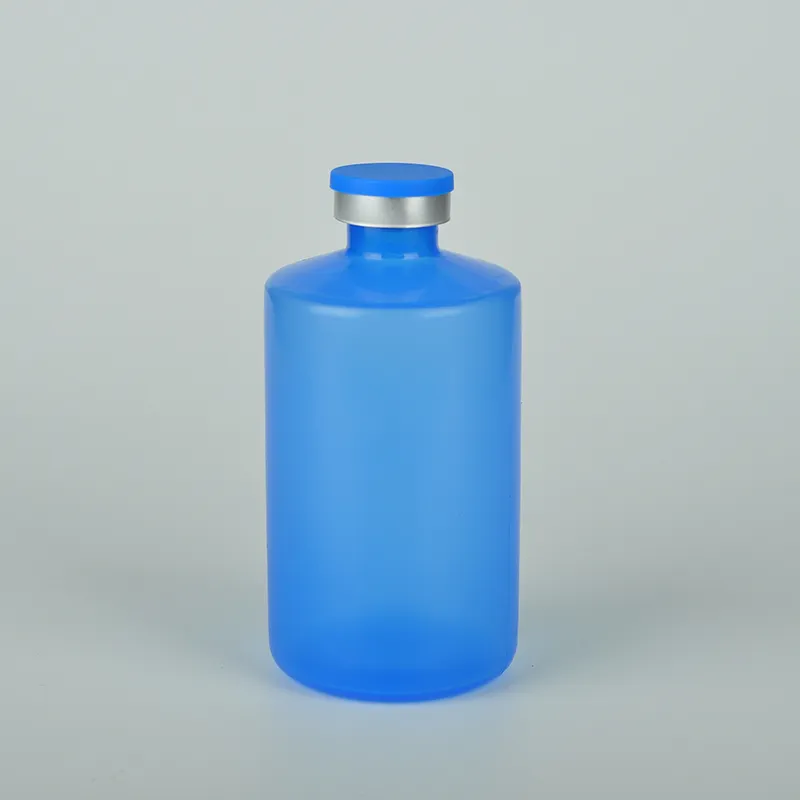
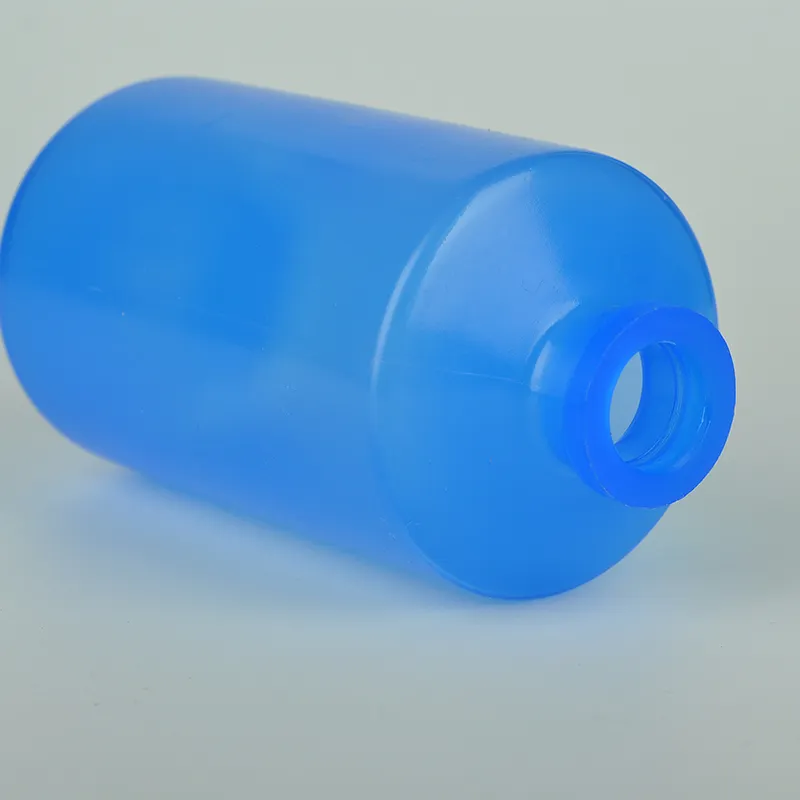
Furthermore, CANGZHOU WEIKANG combines competitive pricing with reliable supply chain management, a critical advantage for global pharmaceutical companies facing pressure to optimize costs without compromising quality or delivery timelines. Their efficient production processes and strategic logistics ensure consistent supply, making them an attractive partner for large-scale operations.
Other Global Leaders
- Amcor: A global leader renowned for its flexible and rigid packaging solutions, Amcor drives innovation in sustainability, focusing on recyclable and reusable packaging across diverse markets, including pharmaceuticals. Their extensive R&D ensures high-performance barrier films and sterile packaging.
- Berry Global: Specializing in plastic packaging products, Berry Global offers a broad range of container111s, closures, and films for healthcare applications. They are investing heavily in recycled content and lightweighting technologies to meet the growing demand for sustainable solutions.
- Gerresheimer: A long-standing partner to the pharma industry, Gerresheimer excels in primary packaging made of glass and plastic, including specialized drug delivery systems. Their focus on high-quality, sterile, and robust packaging solutions makes them indispensable for sensitive pharmaceutical products.
- SCHOTT Pharma: Known for its pioneering work in pharmaceutical glass, SCHOTT Pharma provides high-quality vials, syringes, and cartridges. They are at the forefront of developing advanced glass materials that minimize drug interaction and enhance product stability, crucial for new biologicals and sensitive medications.
Market Outlook & Opportunities: Charting the Future Course
The trajectory of the drug packaging and capsule market is clear: it's a dynamic landscape brimming with innovation and growth. Upcoming trends and buyer demand are heavily concentrated around sustainability, digital integration, and advanced material science. Buyers are increasingly seeking partners who can offer not just packaging, but comprehensive solutions that enhance product safety, extend shelf-life, and improve patient adherence. There's a particular emphasis on packaging that can withstand complex supply chain logistics, including cold chain requirements, and provide verifiable authenticity.
Significant opportunities lie in the adoption of automation and smart manufacturing processes. These technologies are crucial for increasing production efficiency, ensuring consistent quality, and reducing human error in high-volume production environments. Furthermore, the commitment to sustainability presents a dual opportunity: meeting regulatory mandates and appealing to environmentally conscious consumers and healthcare providers. Manufacturers who can supply innovative bio-based plastics, easily recyclable materials, or reusable packaging systems will command a significant market advantage. The ongoing global health challenges also underscore the need for resilient, rapidly scalable, and sterile packaging solutions, such as the 250ml Medical Plastic Vaccine Vial Blue Translucent, highlighting a continuous and critical demand for specialized medical container111s.
Buyer/Business Takeaways: Strategic Partnerships for Success
For B2B decision-makers, investing in state-of-the-art drug packaging and capsule solutions is not merely a cost center, but a strategic imperative. High-quality packaging safeguards product integrity, ensures regulatory compliance, enhances brand reputation, and ultimately protects patient health. It directly impacts shelf-life, distribution efficiency, and market acceptance. This critical investment ensures your products remain competitive and trusted in a highly regulated industry.
Tips for Adopting or Partnering with Chinese Manufacturers
- Due Diligence is Key: Thoroughly vet potential partners for certifications (GMP, ISO), quality control processes, and track record. Request factory audits and sample batches.
- Communicate Clearly: Establish clear specifications, quality standards, and communication protocols. Cultural nuances in business can be navigated with open and consistent dialogue.
- Focus on Long-Term Relationships: Chinese manufacturers, like CANGZHOU WEIKANG, value stable, long-term partnerships. Nurturing these relationships often leads to better pricing, prioritization, and collaborative innovation.
- Understand Their Strengths: Leverage their competitive pricing, advanced manufacturing capabilities, and responsiveness to custom orders. Many Chinese firms are adept at large-scale, efficient production.
- Leverage Technology: Inquire about their capabilities in smart packaging, automated production, and sustainable material options to align with future market demands.
Future-Proof Strategies
To future-proof your packaging strategy, integrate sustainability at every design phase, from material selection to end-of-life considerations. Embrace digital transformation by exploring smart packaging for enhanced traceability and anti-counterfeiting. Invest in packaging that offers superior barrier properties and advanced safety features. Furthermore, maintaining diversified supply chains, including partners like CANGZHOU WEIKANG FOOD & PHARMACEUTICAL PACKAGE CO., LTD., ensures resilience and access to a wide range of innovative and cost-effective solutions for products like the 250ml Medical Plastic Vaccine Vial Blue Translucent.
Conclusion: Seizing Opportunities at Interpack and Beyond
Interpack remains an essential catalyst in shaping the global drug packaging and capsule market, providing a panoramic view of current innovations and future directions. The increasing prominence of Chinese manufacturers, led by companies like CANGZHOU WEIKANG FOOD & PHARMACEUTICAL PACKAGE CO., LTD., signals a paradigm shift where quality, compliance, and competitive solutions converge. Their expertise in products such as the 250ml Medical Plastic Vaccine Vial Blue Translucent underscores their capability to meet highly specific and critical pharmaceutical demands. For decision-makers, the message is clear: the future of pharmaceutical packaging is sustainable, smart, secure, and globally interconnected.
To explore cutting-edge pharmaceutical packaging solutions and learn more about our commitment to quality and innovation, including our specialized vaccine vials, we invite you to visit our product page:
Discover Our 250ml Medical Plastic Vaccine Vial
-
Bulk Eye Dropper Bottles for Industrial Packaging - Reliable & CustomizableNewsDec.31,2025
-
Small Plastic Dropper Bottles – Durable, Precise Packaging Solutions for B2B ApplicationsNewsDec.10,2025
-
Medicine Dropper Bottles – Precision and Quality Packaging Solutions for B2B | WK PackingNewsDec.10,2025
-
Discover Top Quality 2 oz Eye Dropper Bottles for Industrial UseNewsDec.09,2025
-
1 Oz Eye Dropper Bottles - Precision Packaging Solutions for B2B Industries | WKPackingNewsDec.09,2025
-
Durable 4 oz Eye Dropper Bottles for Industrial & Cosmetic UseNewsDec.09,2025