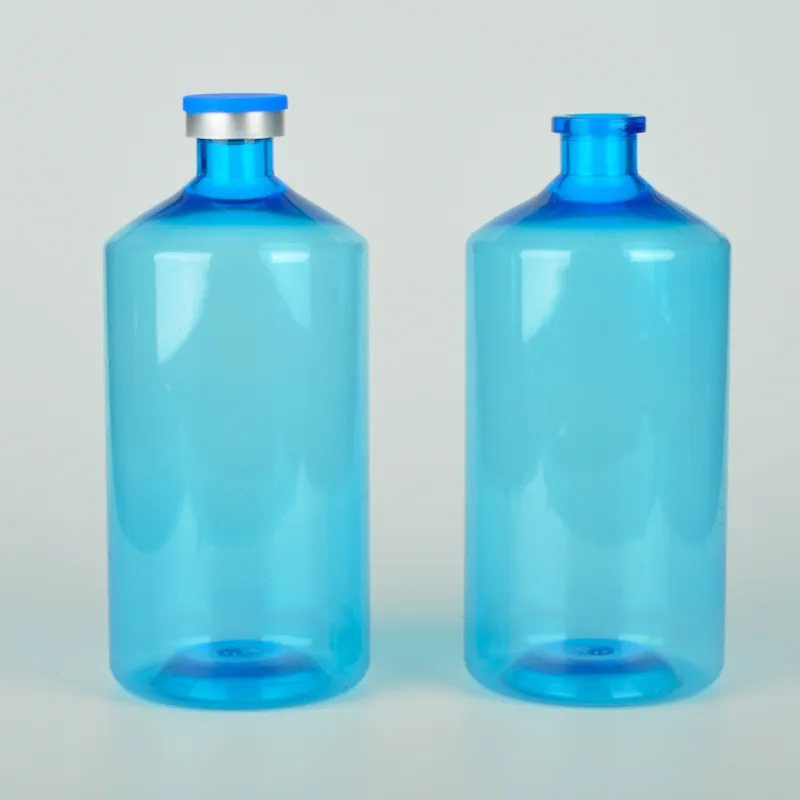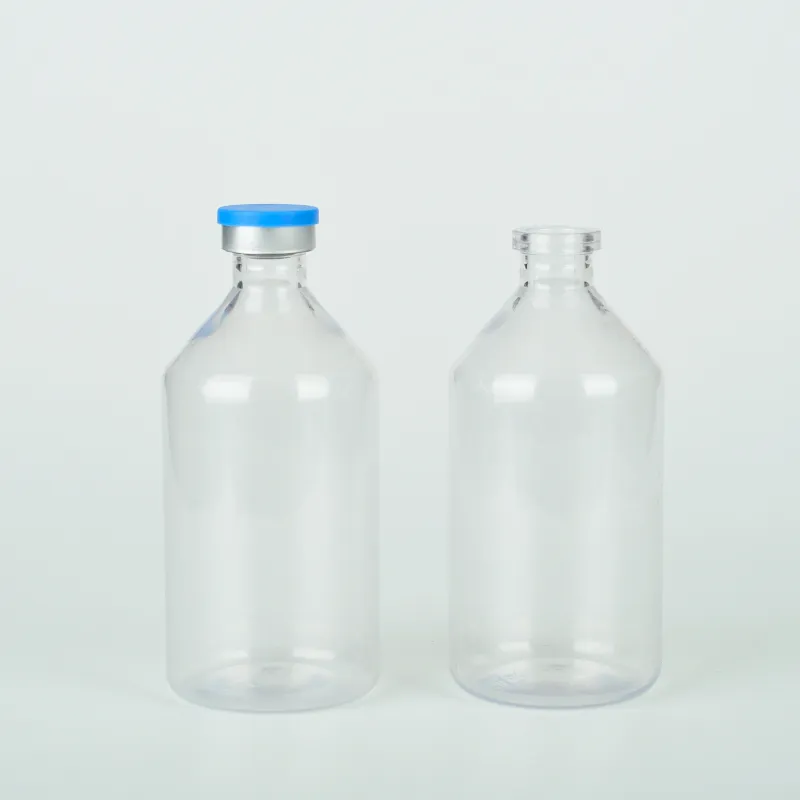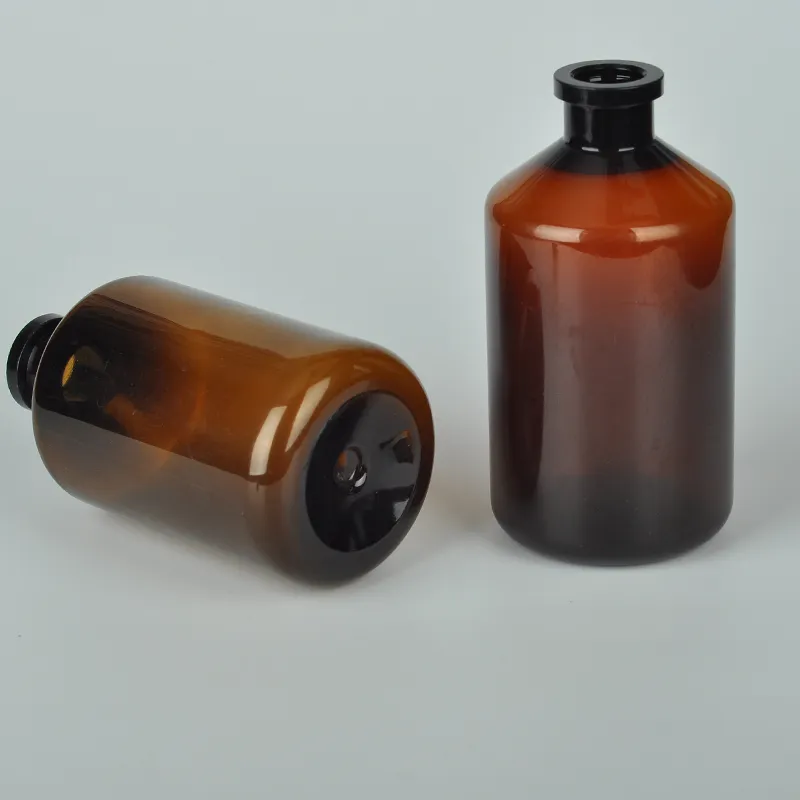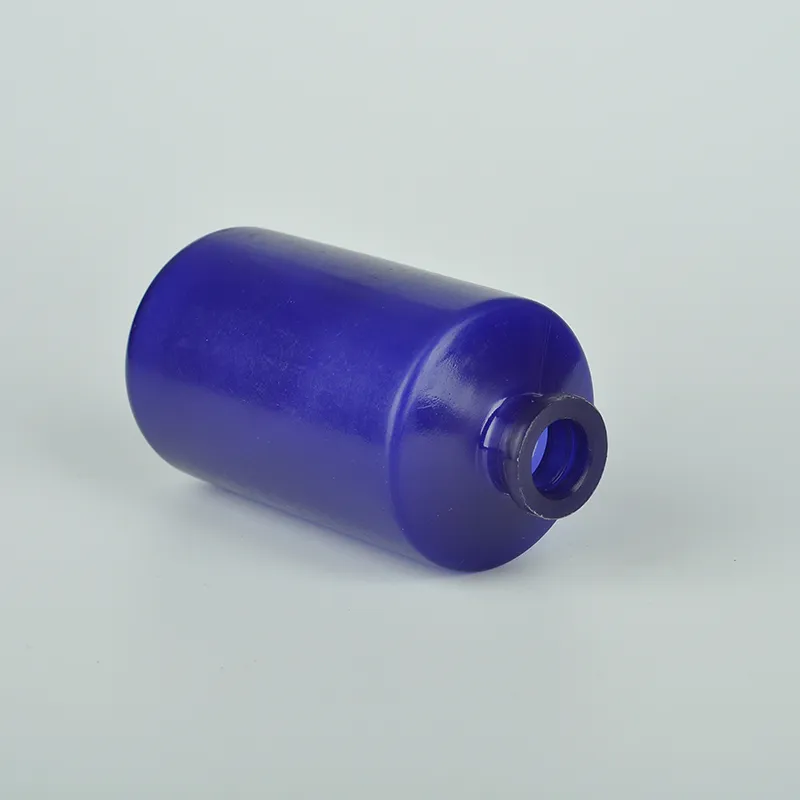
Pharmaceutical 10ml-20ml Brown PET Plastic Liquid Syrup Bottle-Cangzhou Weikang Food & Pharmaceutical Package Co., Ltd.|Leak-proof&Chemical Resistance
Product Overview
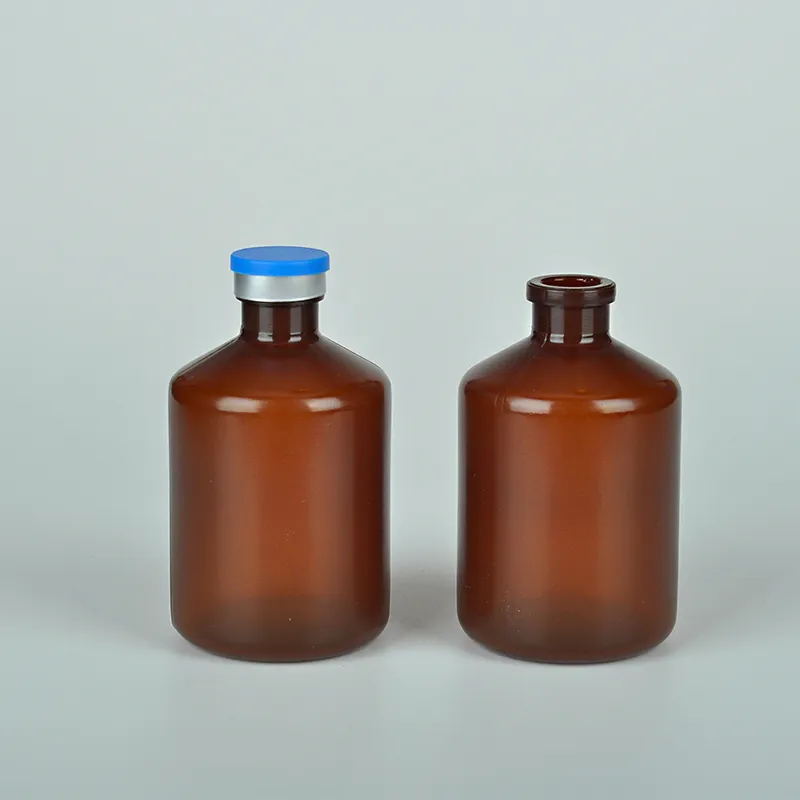
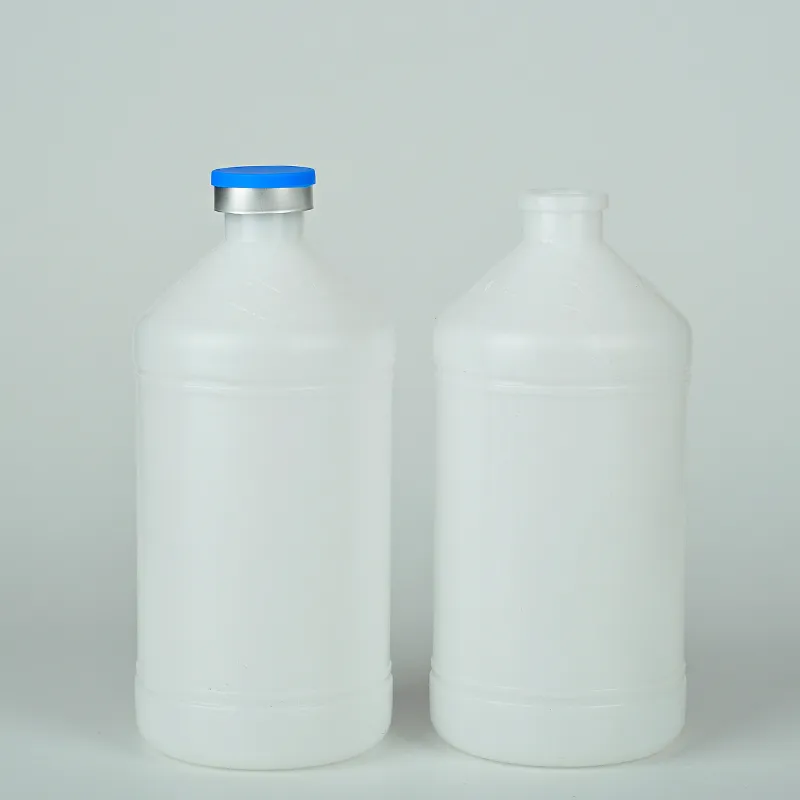
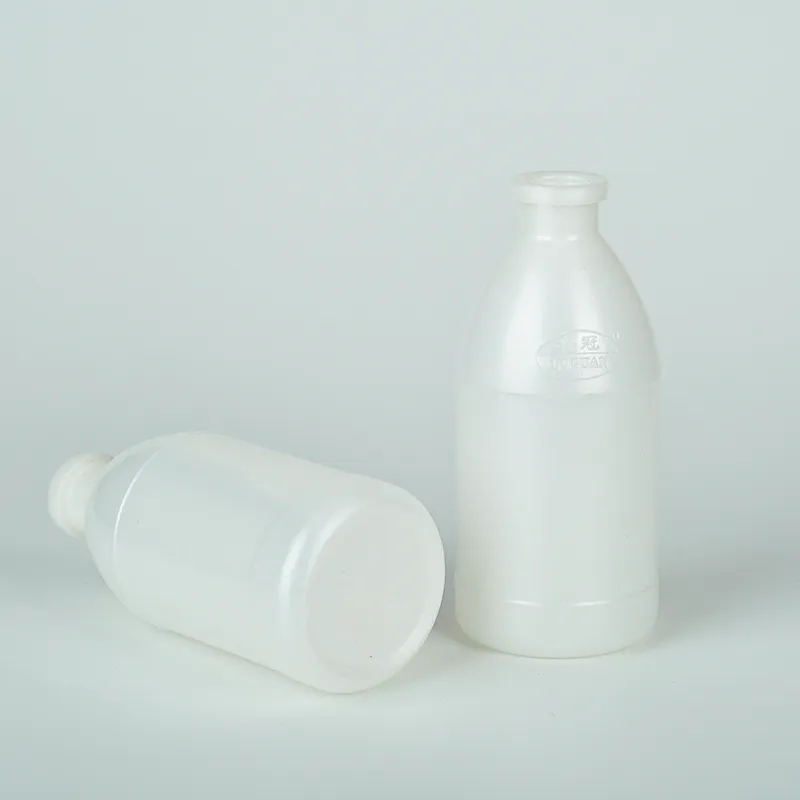
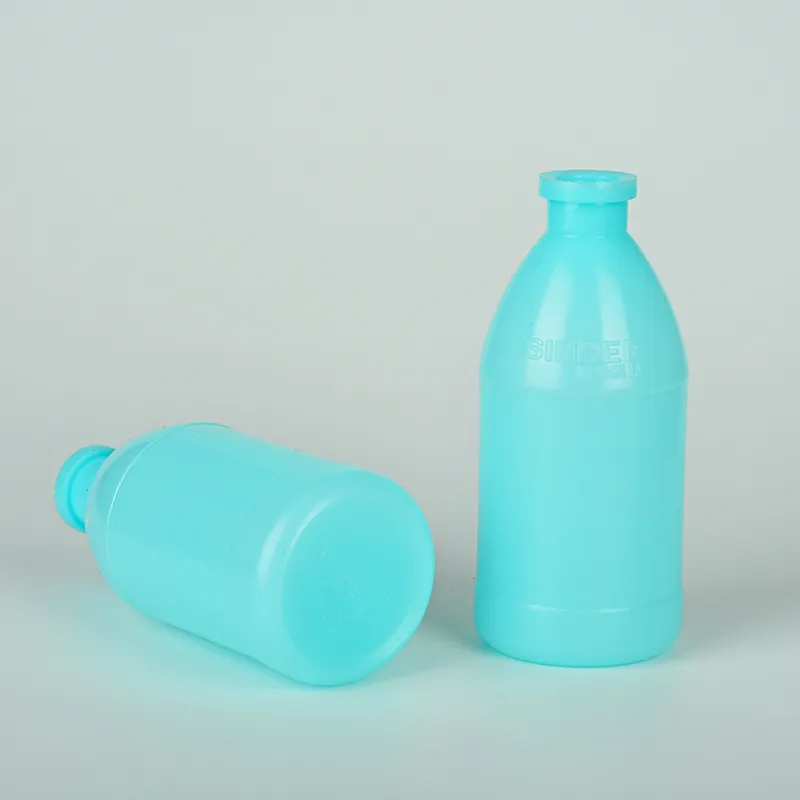
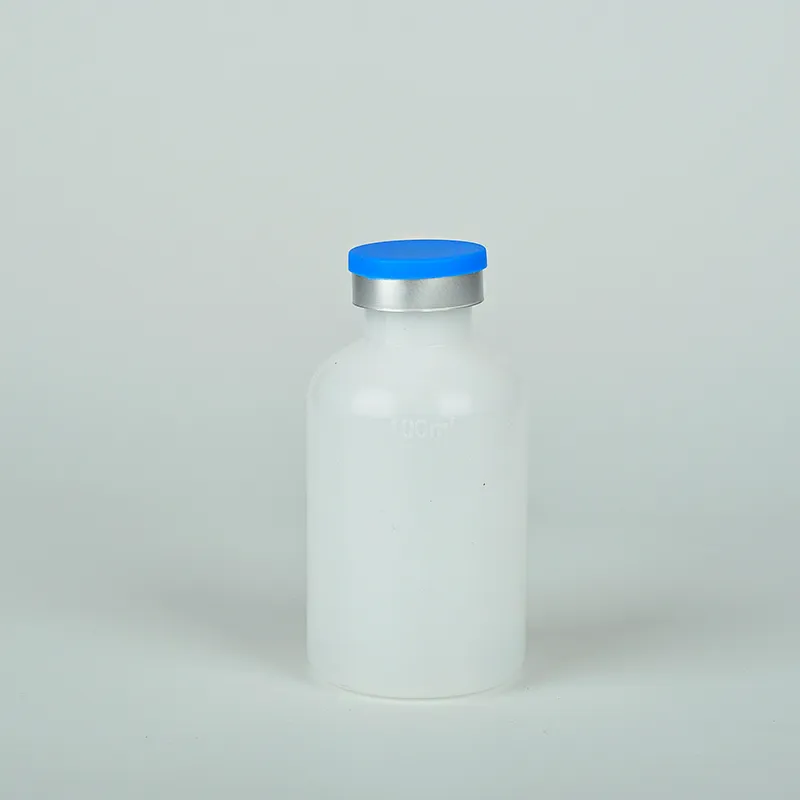
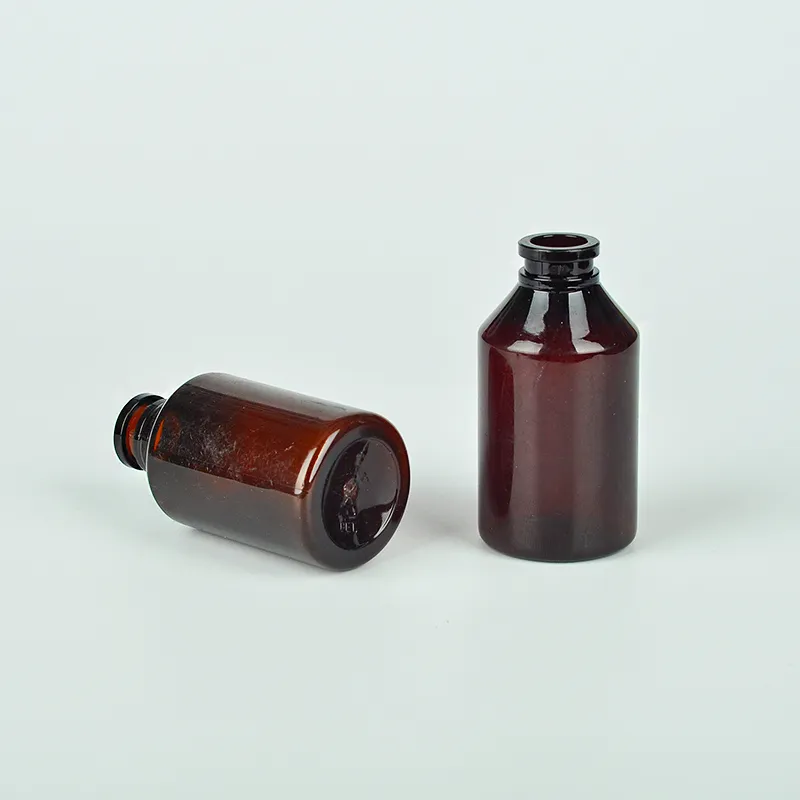
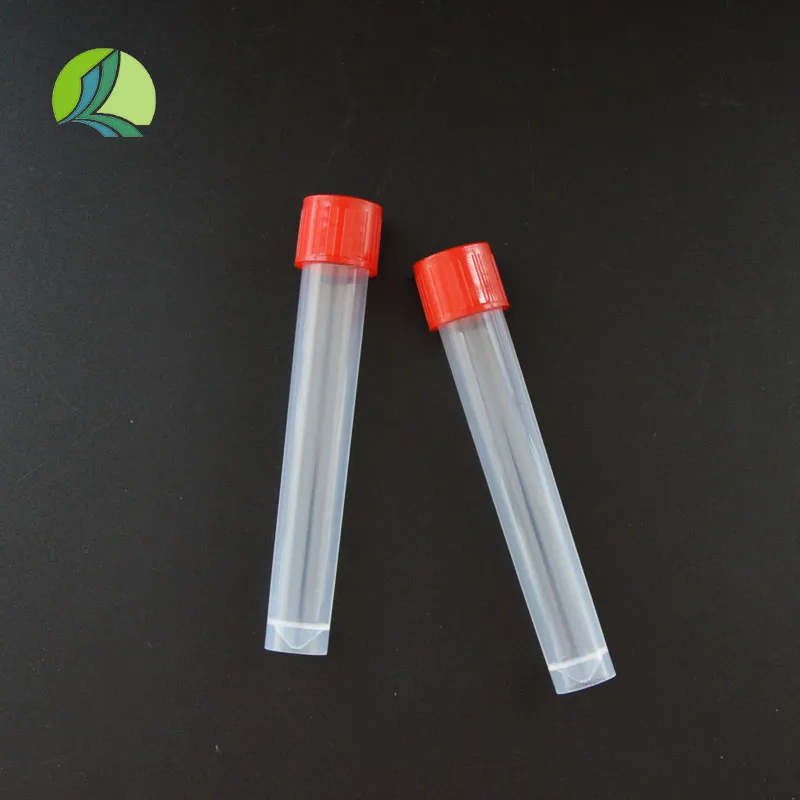
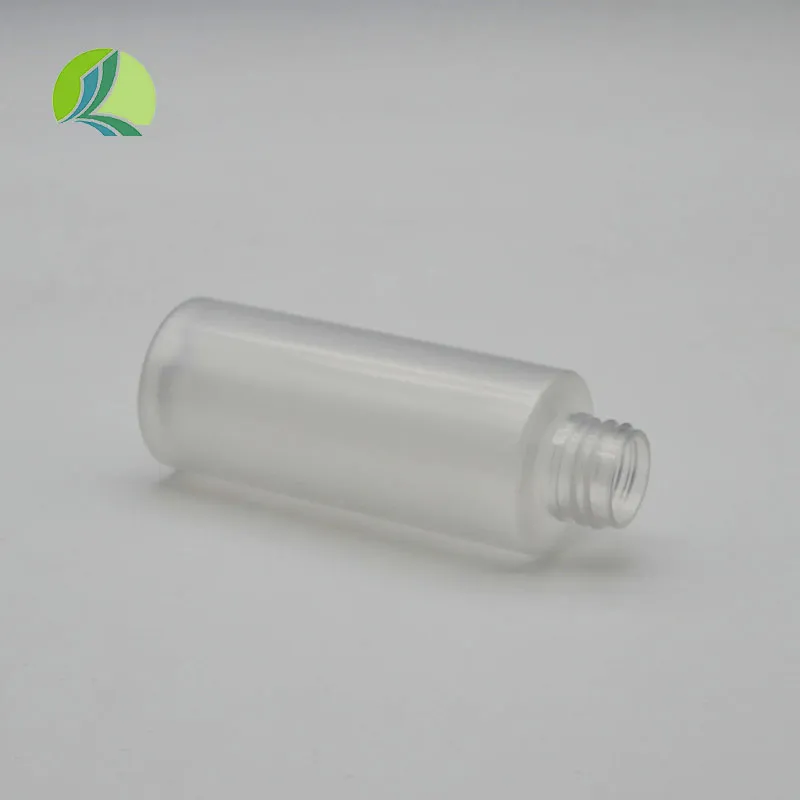
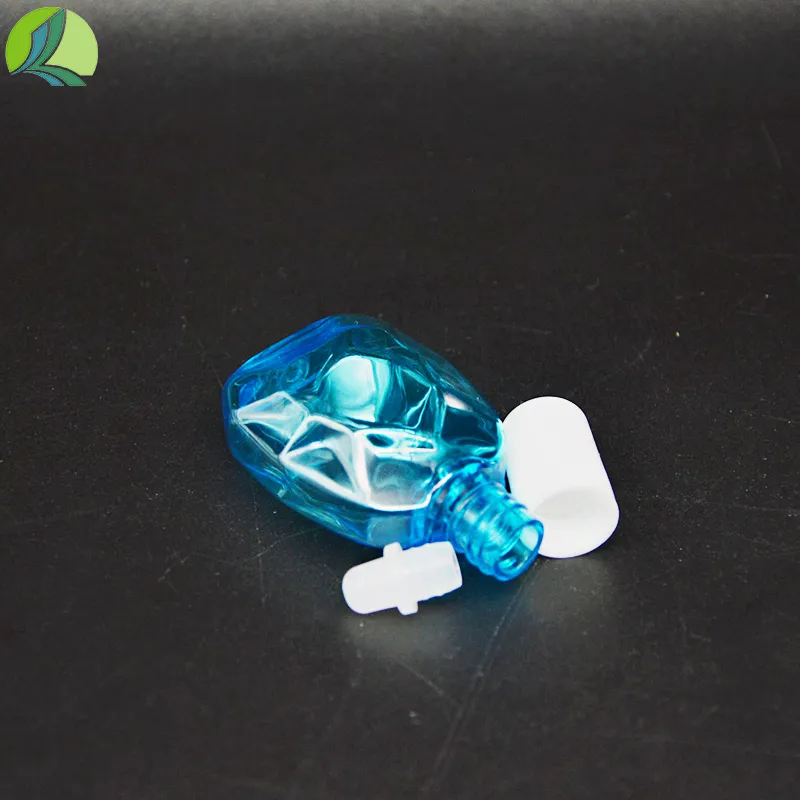
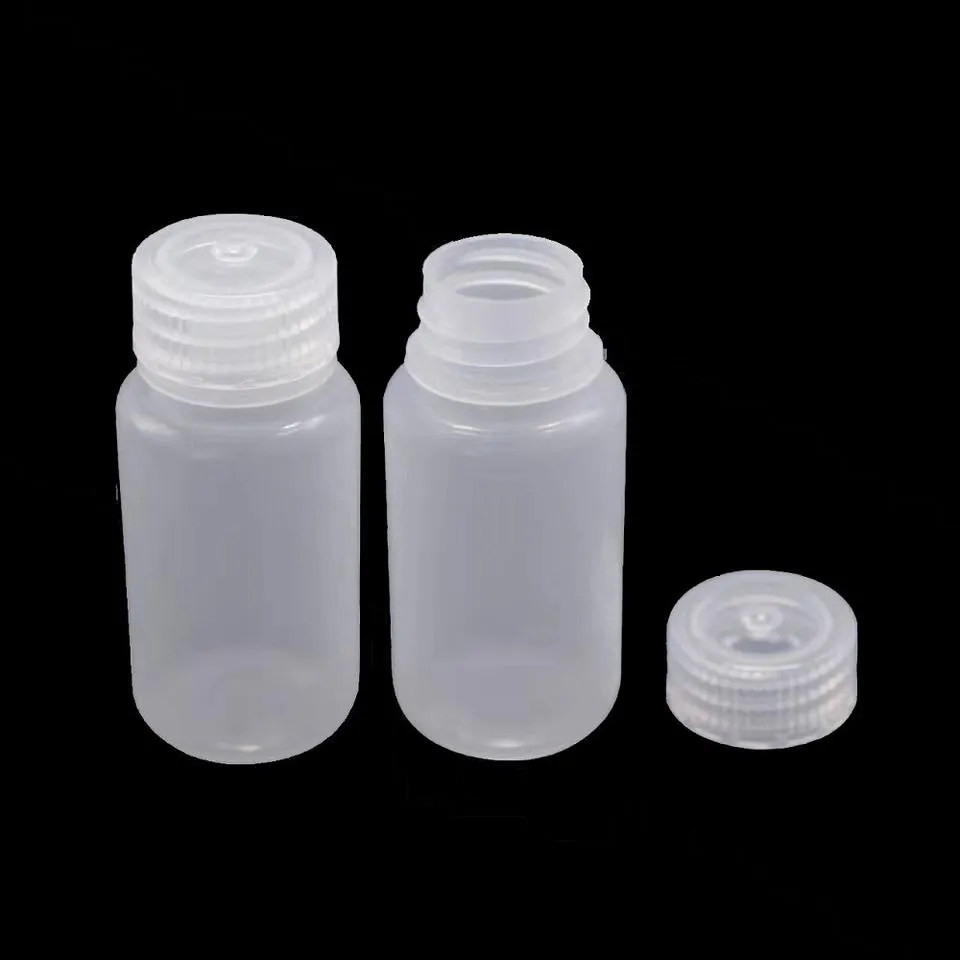
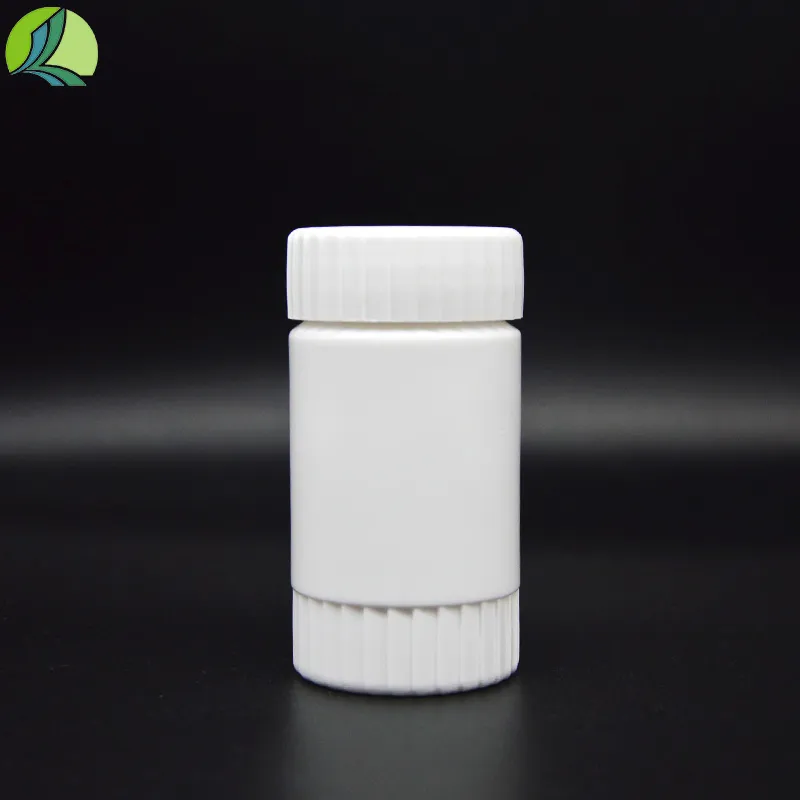
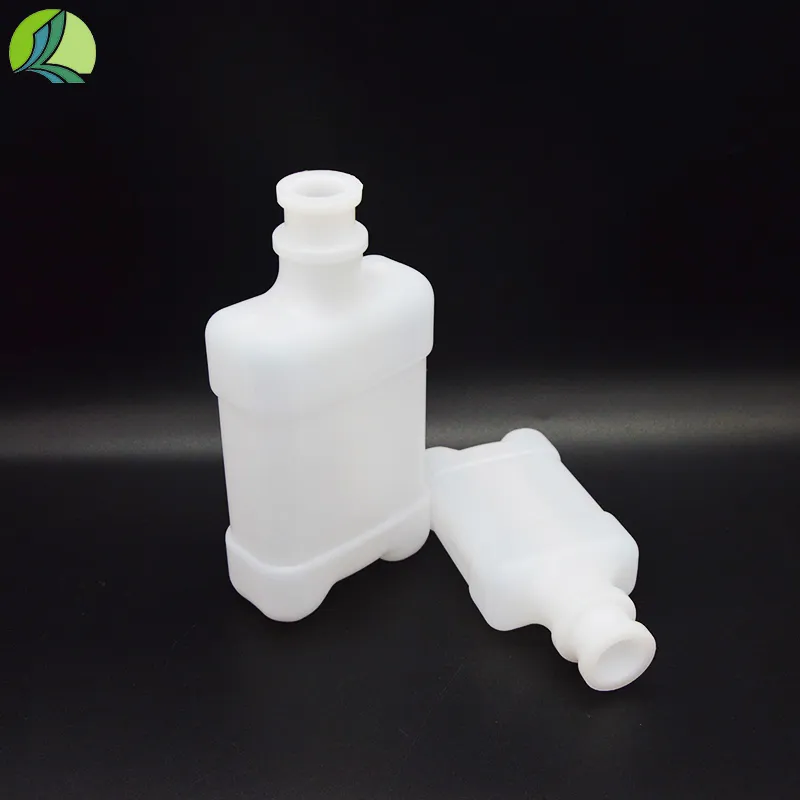
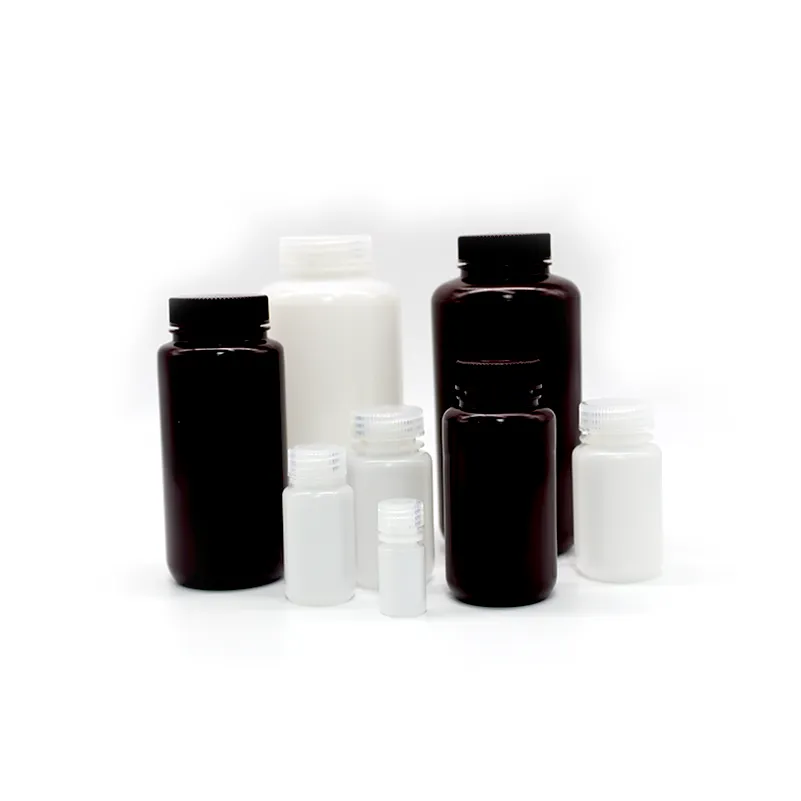
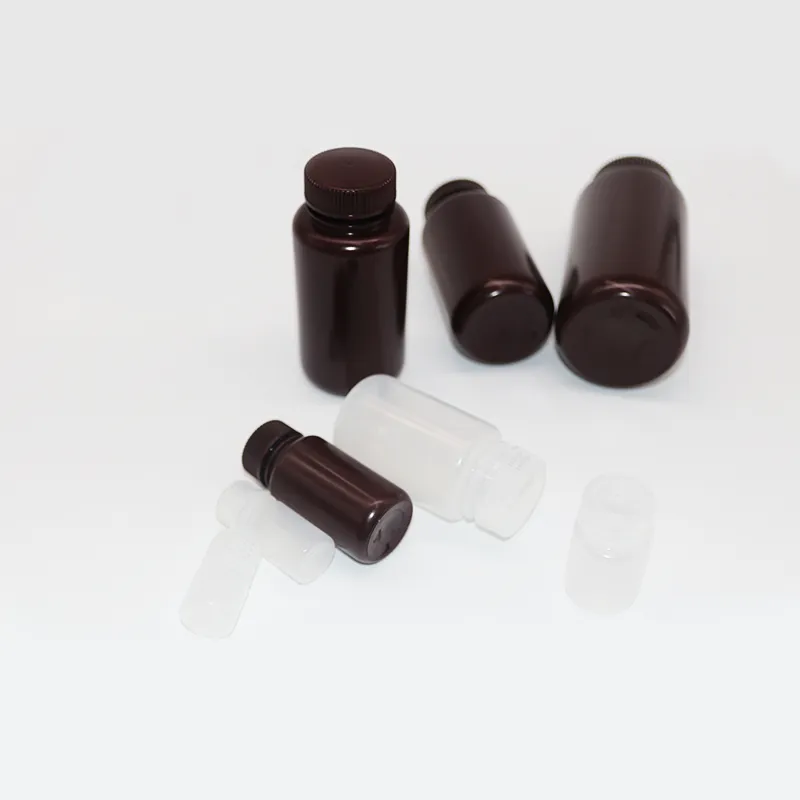
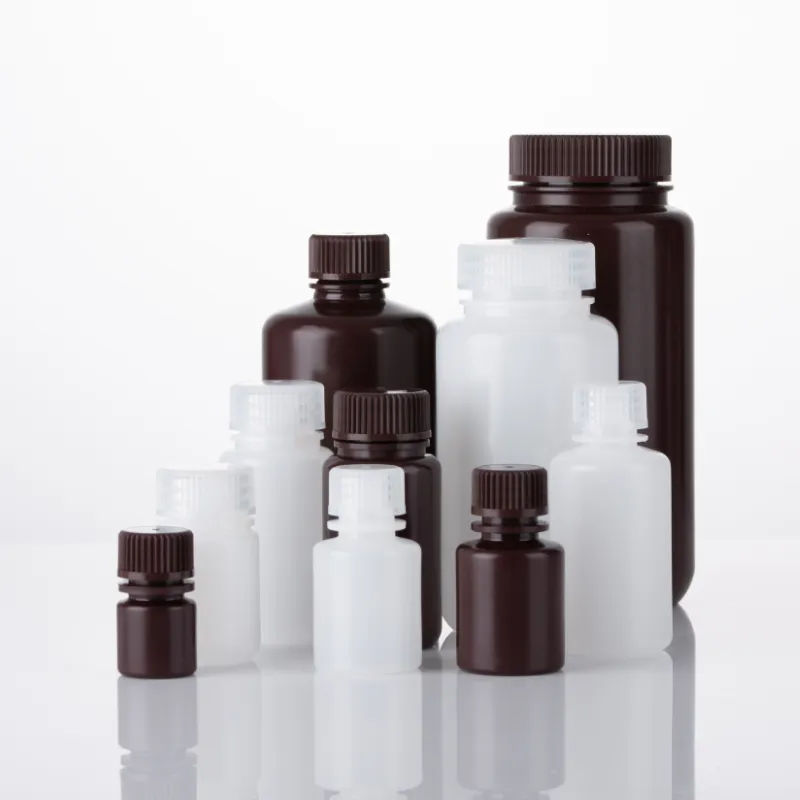
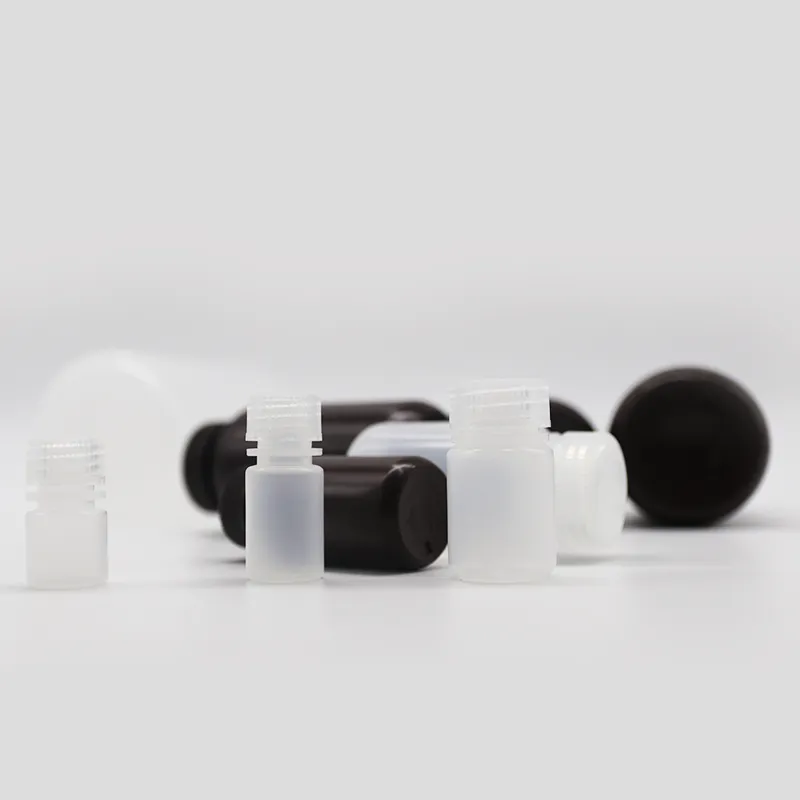
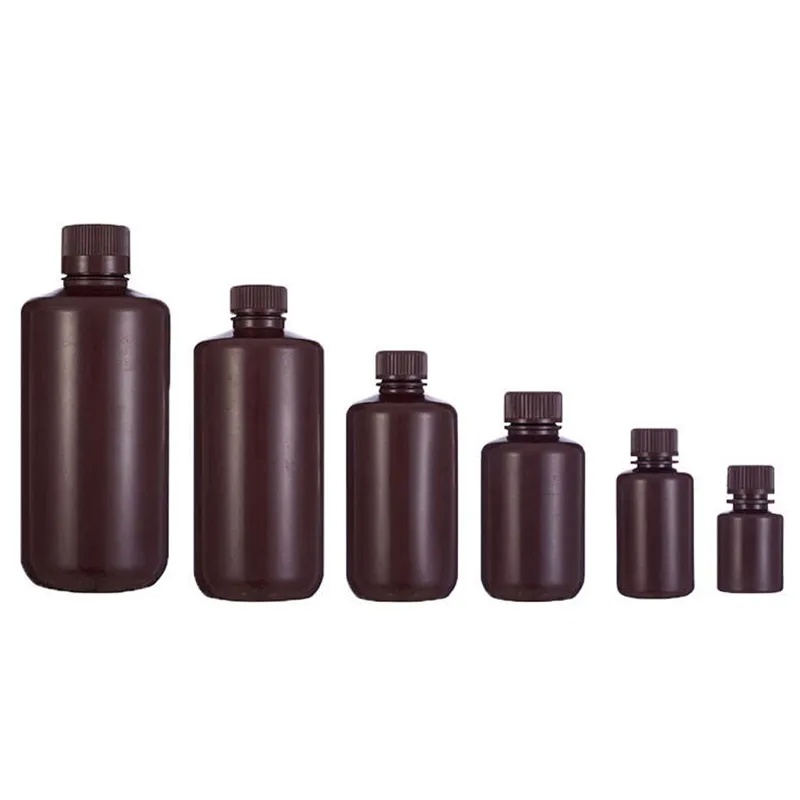
The Pharmaceutical 10ml-20ml Brown PET Plastic Liquid Syrup Bottle is a specialized packaging solution designed for the safe storage and transportation of liquid medications and reagents. Engineered with precision, this bottle combines durability, chemical resistance, and user-friendly features to meet the demands of the pharmaceutical and laboratory industries. Its design ensures long-term storage, leak-proof performance, and adaptability to various applications, making it an essential component in modern medicine and diagnostics.
Key Design Features
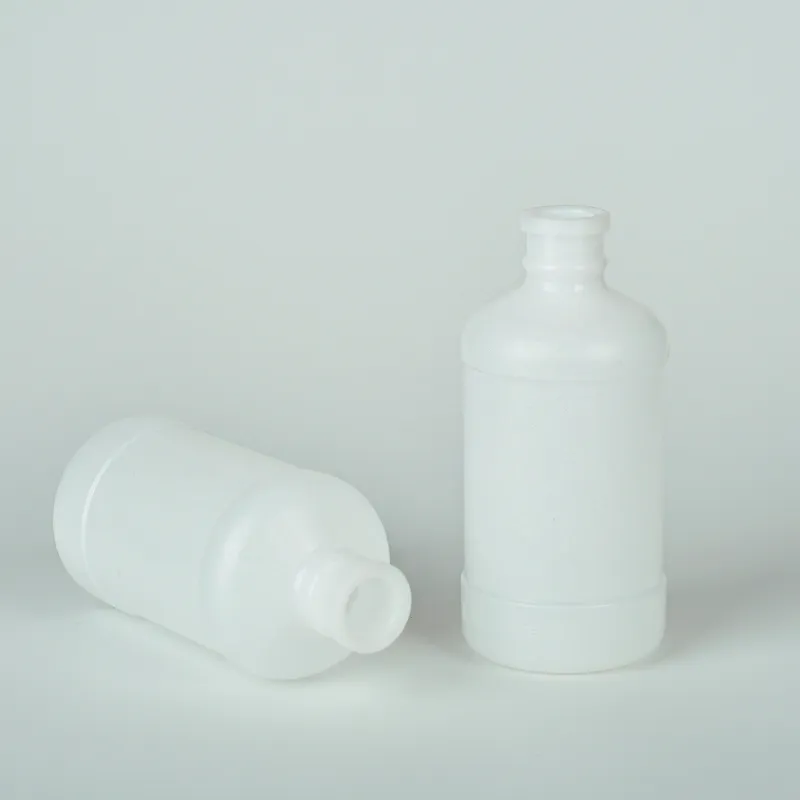
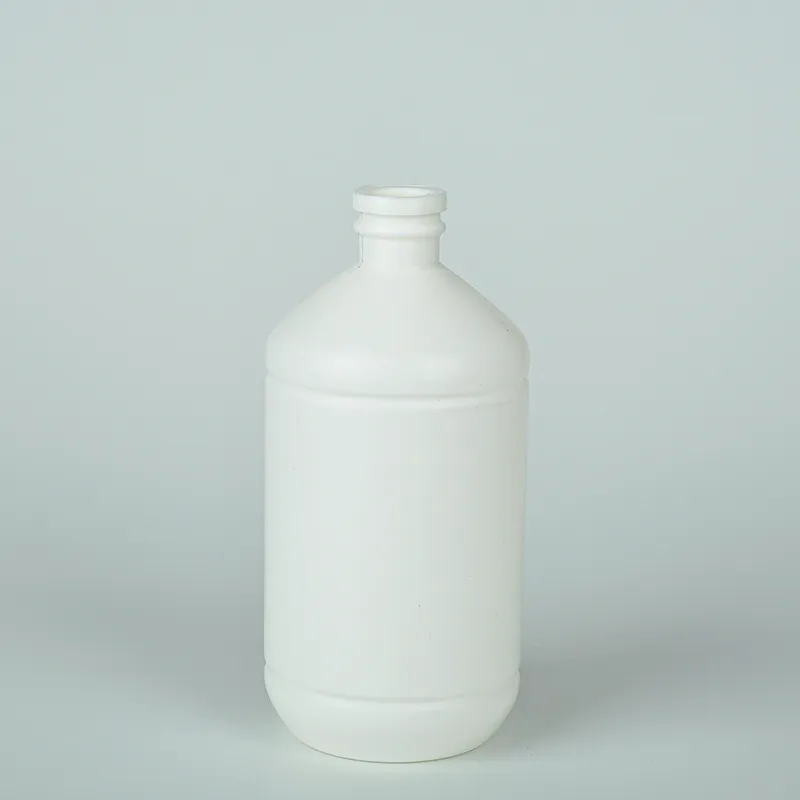
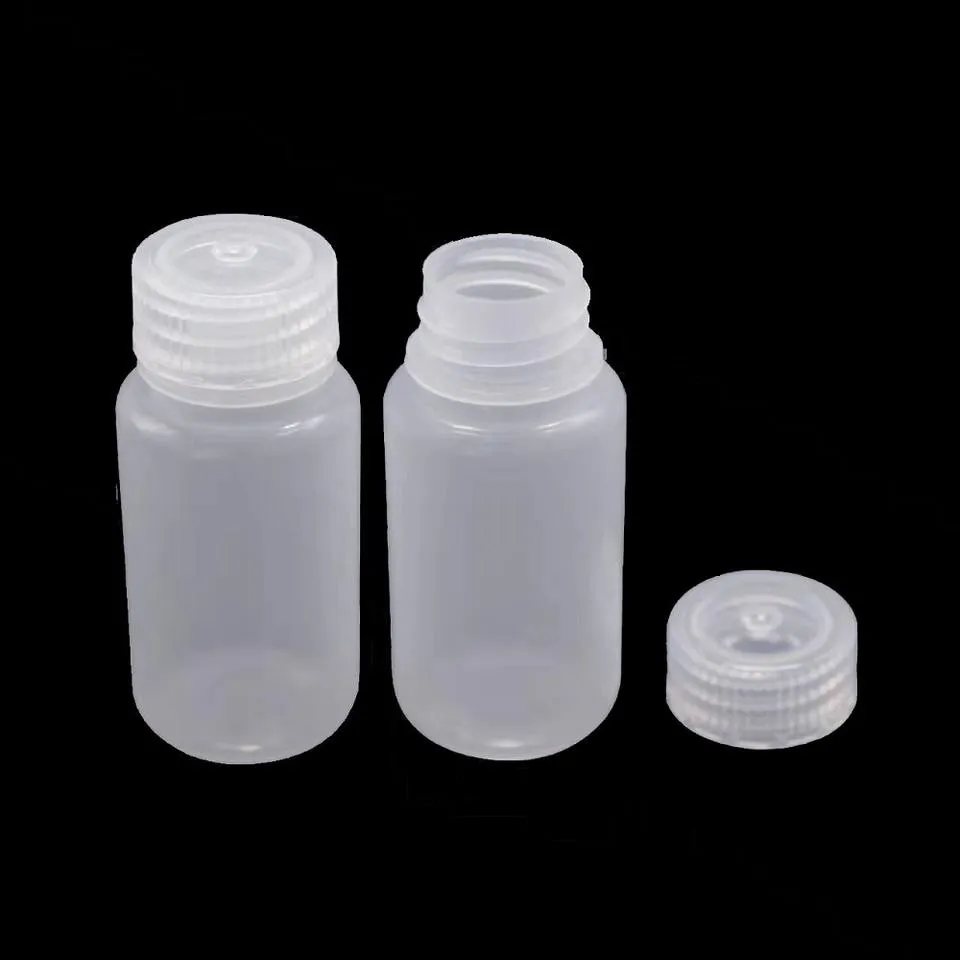
- Special Bottle Mouth Design: The bottle’s unique mouth design allows for secure cap spinning without the need for an inner pad, minimizing the risk of liquid leakage. This feature is particularly critical for handling sensitive pharmaceutical solutions.
- High-Density Polyethylene (HDPE) Body: The bottle body is crafted from high-density polyethylene, a material renowned for its strength, resistance to impact, and ability to withstand extreme temperatures. This ensures the bottle remains intact during storage, even in frozen conditions.
- High-Permeability Polypropylene Cap: The screw cap is made of high-permeability polypropylene, which offers excellent chemical resistance and compatibility with sterilization methods such as radiation. This makes the bottle suitable for use in sterile environments.
- Customization Options: For clients with specific requirements, the manufacturer offers tailored designs, including custom bottle shapes and the ability to incorporate invisible logos. This flexibility allows businesses to align the packaging with their brand identity.
Technical Specifications
| Parameter | Details |
|---|---|
| Material | HDPE (Bottle Body), PP (Cap) |
| Capacity | 10ml, 20ml |
| Color | Brown PET |
| Sealing Mechanism | Interference Fit Design (No Gasket Required) |
| Temperature Resistance | Low-Temperature Storage (Freezing Compatible) |
| Chemical Resistance | Resists a wide range of reagents (pH 5.5–9.0) |
| Customization | Available for bespoke designs and logos |
Product Advantages
1. Leak-Proof and Secure Sealing
The bottle’s interference fit design ensures airtight sealing without the need for an inner gasket. This eliminates the risk of contamination and leakage, making it ideal for storing sensitive liquids such as diagnostic reagents and pharmaceutical solutions.
2. Long-Term Storage and Stability
Manufactured to withstand prolonged exposure to low temperatures, the bottle remains structurally intact even when frozen. This feature is crucial for pharmaceutical companies that require long-term storage of liquid medications and reagents. The HDPE material also prevents degradation over time, maintaining the integrity of the contents.
3. Chemical Resistance and Sterilization Compatibility
The combination of HDPE and PP materials ensures the bottle is resistant to a wide range of chemicals, including common reagents used in laboratories. Additionally, the cap can be sterilized via radiation, making it suitable for use in sterile environments. This versatility is essential for applications in healthcare, research, and industrial settings.
4. Customization for Branding and Functionality
The manufacturer offers custom bottle designs to meet specific client needs. This includes the option to add invisible logos, which enhances brand visibility without compromising the bottle’s aesthetic or functionality. Custom shapes and sizes can also be developed, providing a tailored solution for unique packaging requirements.
Applications and Use Cases
1. Pharmaceutical Packaging
The bottle is widely used for packaging liquid medications, including syrups, oral solutions, and injectable preparations. Its leak-proof design and chemical resistance make it a reliable choice for storing drugs that require precise dosing and protection from environmental factors.
2. Diagnostic Reagents
Designed for use in in vitro diagnostic applications, the bottle is suitable for storing reagents used in laboratory testing. Its compatibility with pH levels between 5.5 and 9.0 ensures it can hold a variety of chemical solutions without compromising their stability.
3. Food and Beverage Industry
While primarily designed for pharmaceutical use, the bottle’s durability and safety make it suitable for packaging food-grade liquids. Its ability to resist contamination and maintain product quality aligns with the stringent standards of the food industry.
4. Industrial and Chemical Storage
The bottle’s resistance to extreme temperatures and chemicals makes it ideal for storing industrial solvents, cleaning agents, and other chemical solutions. Its robust construction ensures it can handle demanding environments without degradation.
Company Background: Cangzhou Weikang Food & Pharmaceutical Package Co., Ltd.
Based in Cangzhou, China, Cangzhou Weikang Food & Pharmaceutical Package Co., Ltd. is a leading manufacturer of pharmaceutical and food packaging solutions. With years of experience in the industry, the company specializes in producing high-quality container111s that meet international standards for safety and performance. Their commitment to innovation and customization has made them a trusted partner for businesses worldwide.
Industry Expertise and Quality Assurance
Cangzhou Weikang leverages advanced manufacturing techniques and rigorous quality control processes to ensure their products meet the highest standards. The company adheres to global regulations for pharmaceutical packaging, including guidelines from the National Institute of Standards and Technology (NIST), which plays a critical role in developing measurement standards that underpin industrial and scientific advancements.
Commitment to Sustainability
In line with global sustainability efforts, the company prioritizes eco-friendly materials and energy-efficient production methods. Their use of HDPE and PP, which are recyclable and non-toxic, aligns with environmental conservation goals while maintaining product performance.
Conclusion
The Pharmaceutical 10ml-20ml Brown PET Plastic Liquid Syrup Bottle is a versatile and reliable packaging solution that addresses the needs of diverse industries. Its combination of durability, chemical resistance, and customization options makes it an ideal choice for pharmaceutical, diagnostic, and industrial applications. Backed by the expertise of Cangzhou Weikang Food & Pharmaceutical Package Co., Ltd., this product exemplifies the intersection of innovation and quality in modern packaging technology.
References
National Institute of Standards and Technology (NIST). (n.d.). Driving Innovation. Retrieved from https://www.nist.gov
The technical specifications and material standards referenced in this article align with the measurement and quality benchmarks established by NIST, ensuring the product meets rigorous industry requirements.
-
Bulk Eye Dropper Bottles for Industrial Packaging - Reliable & CustomizableNewsDec.31,2025
-
Small Plastic Dropper Bottles – Durable, Precise Packaging Solutions for B2B ApplicationsNewsDec.10,2025
-
Medicine Dropper Bottles – Precision and Quality Packaging Solutions for B2B | WK PackingNewsDec.10,2025
-
Discover Top Quality 2 oz Eye Dropper Bottles for Industrial UseNewsDec.09,2025
-
1 Oz Eye Dropper Bottles - Precision Packaging Solutions for B2B Industries | WKPackingNewsDec.09,2025
-
Durable 4 oz Eye Dropper Bottles for Industrial & Cosmetic UseNewsDec.09,2025