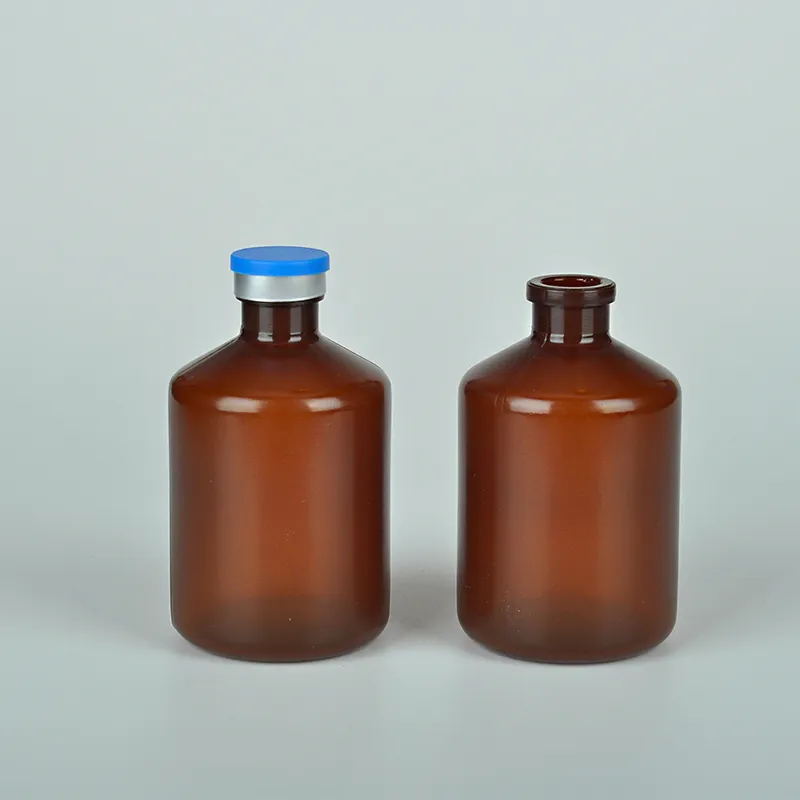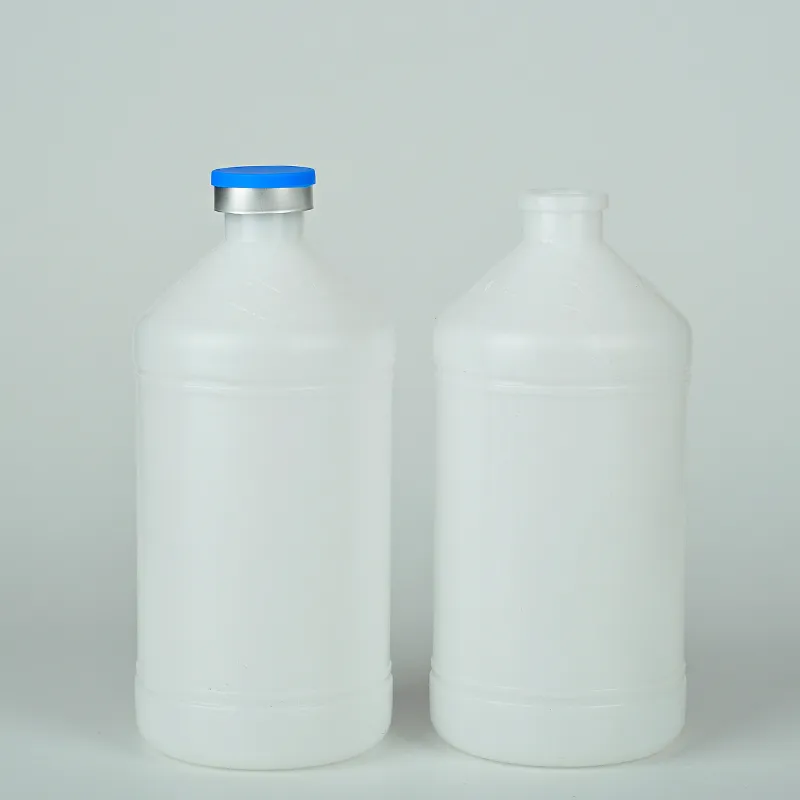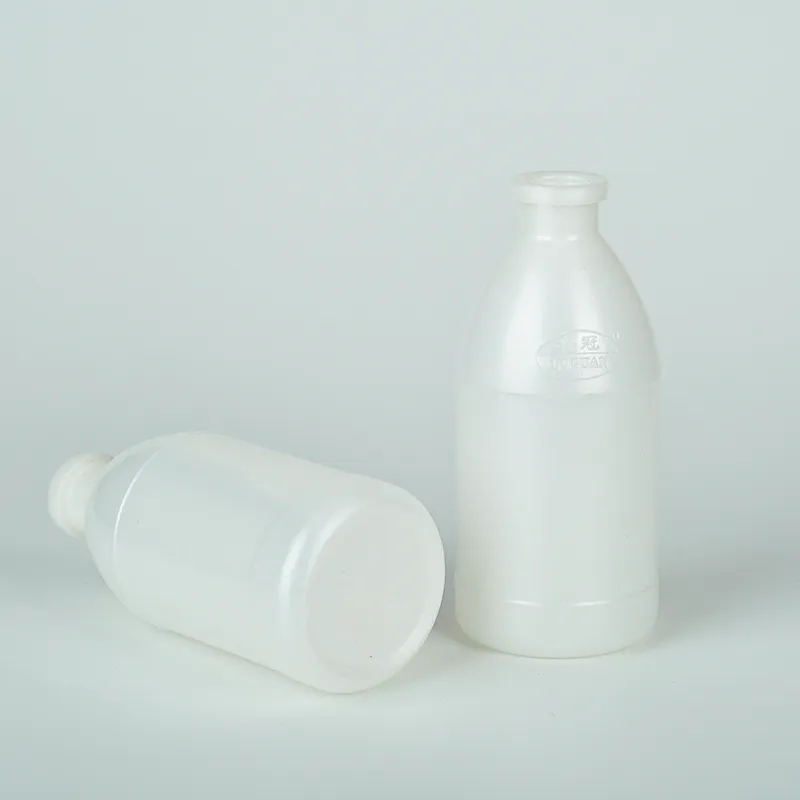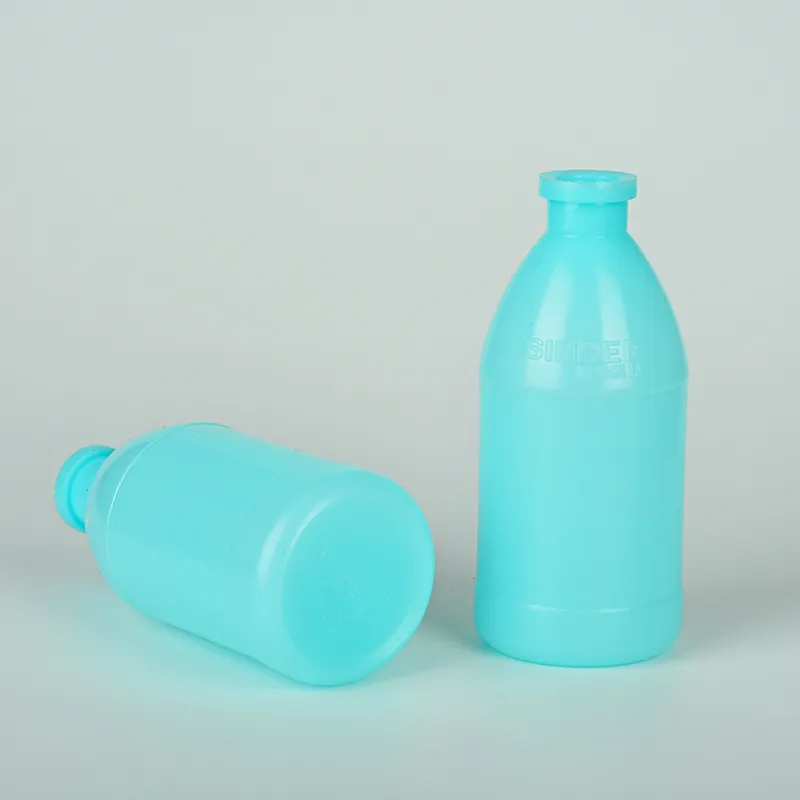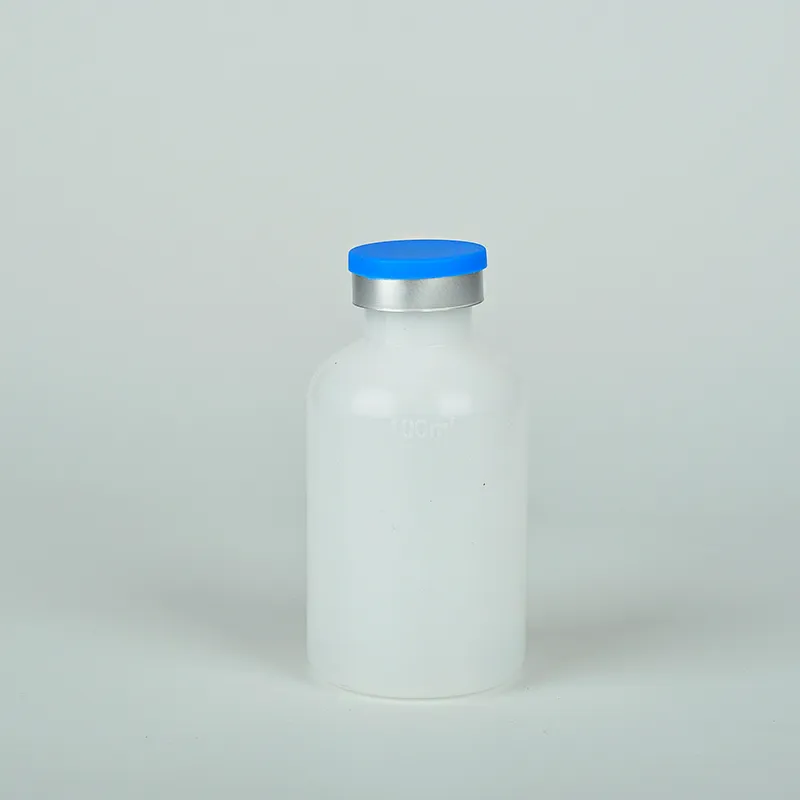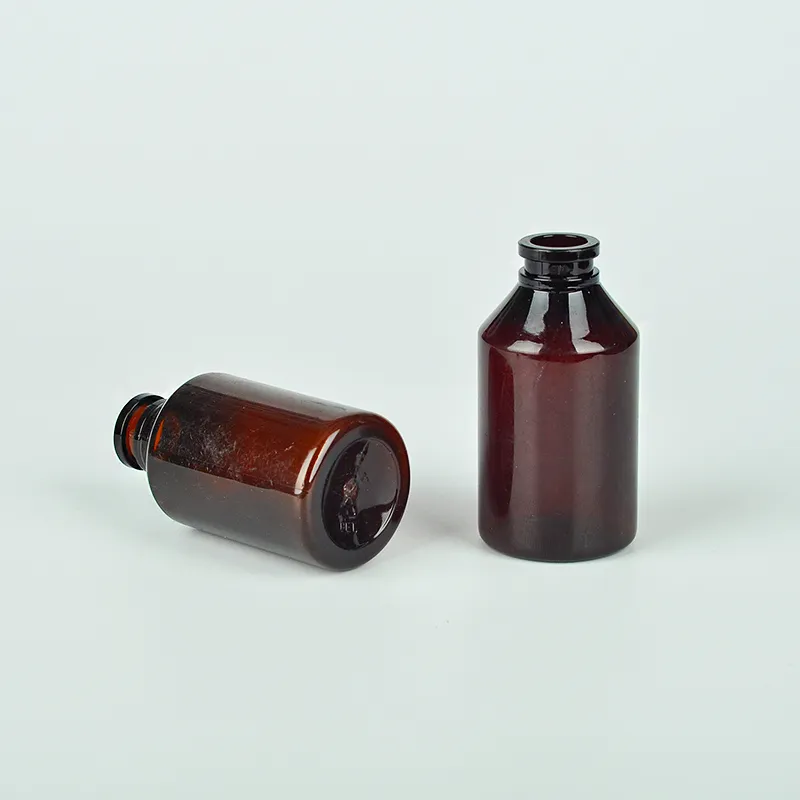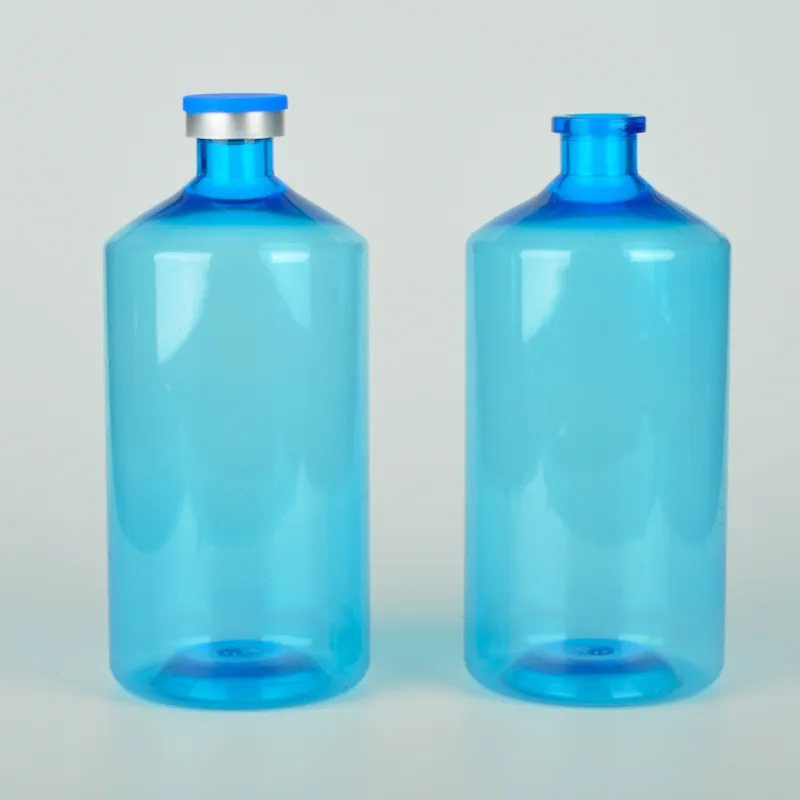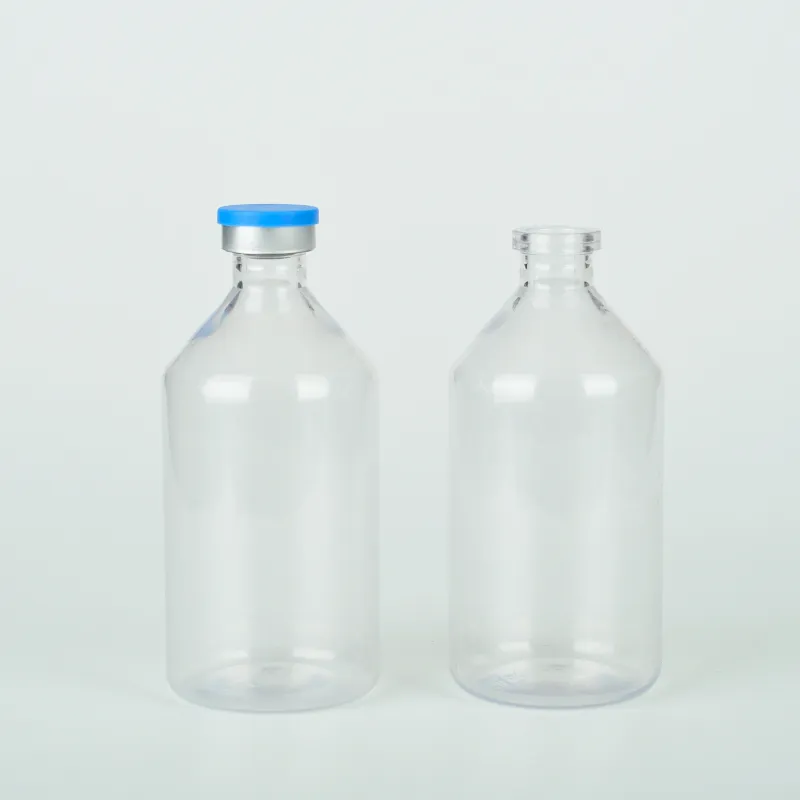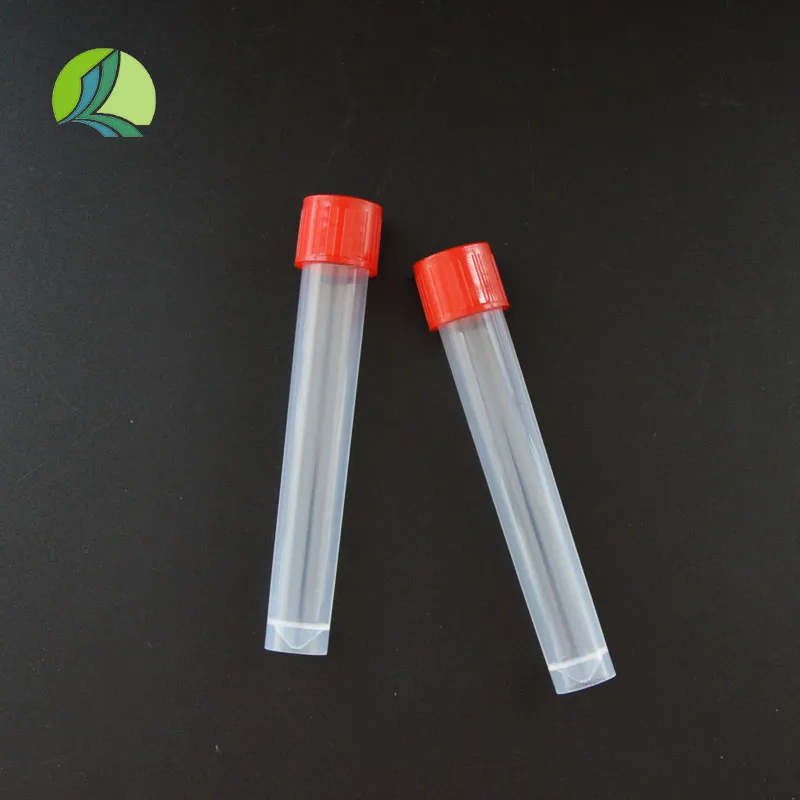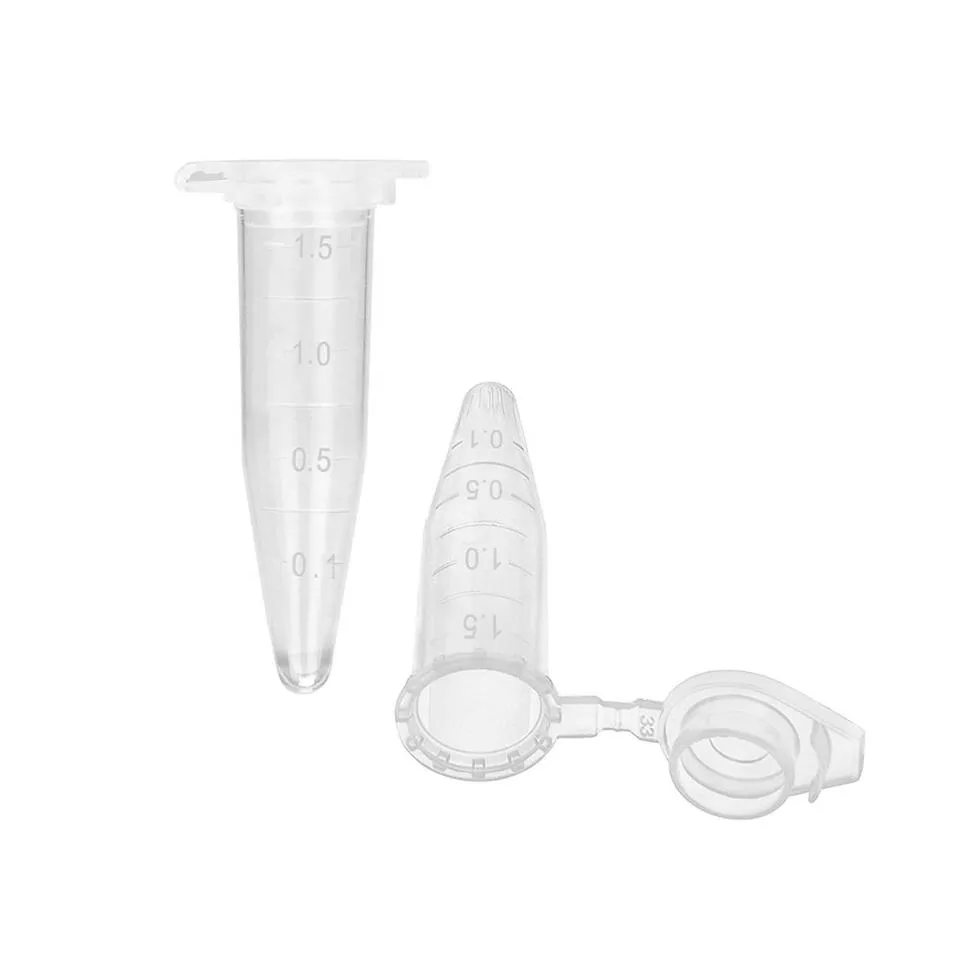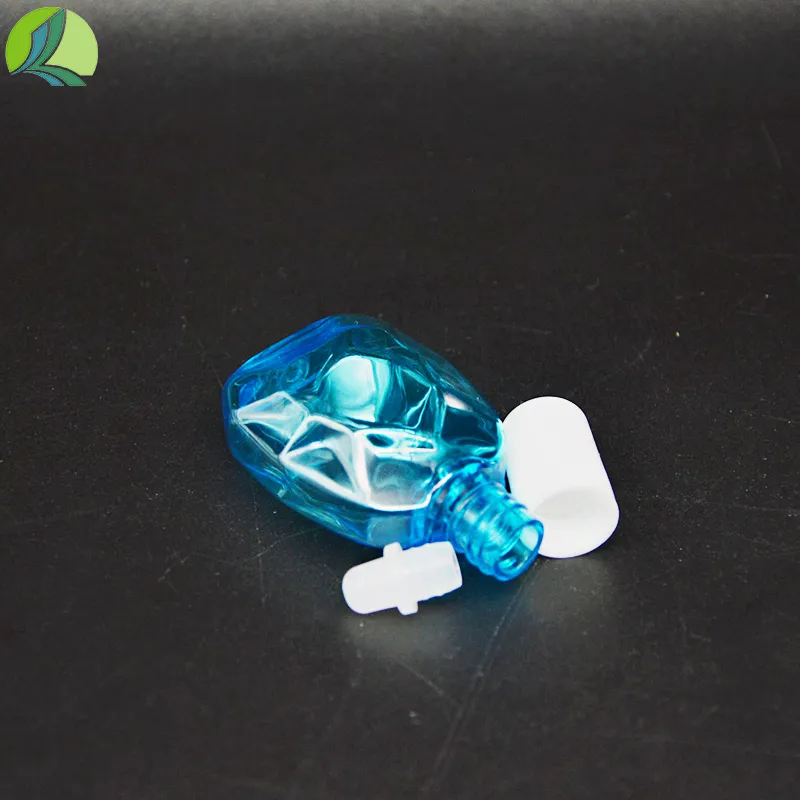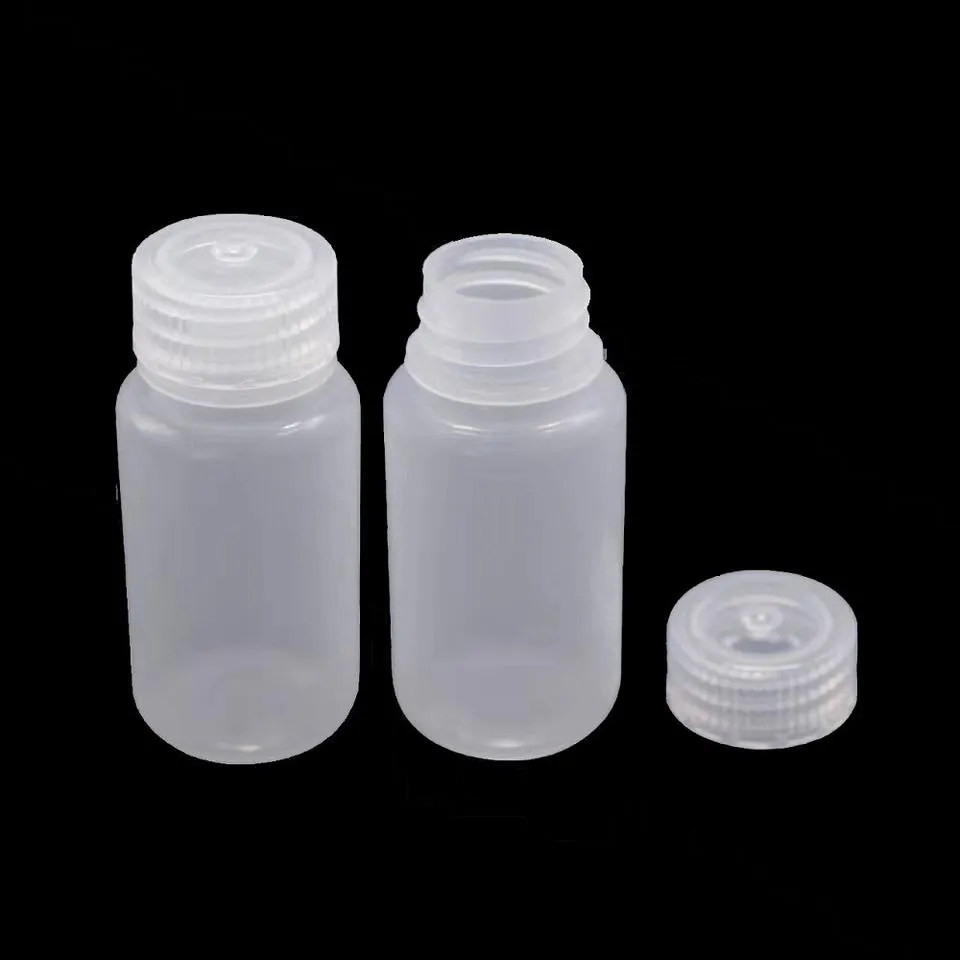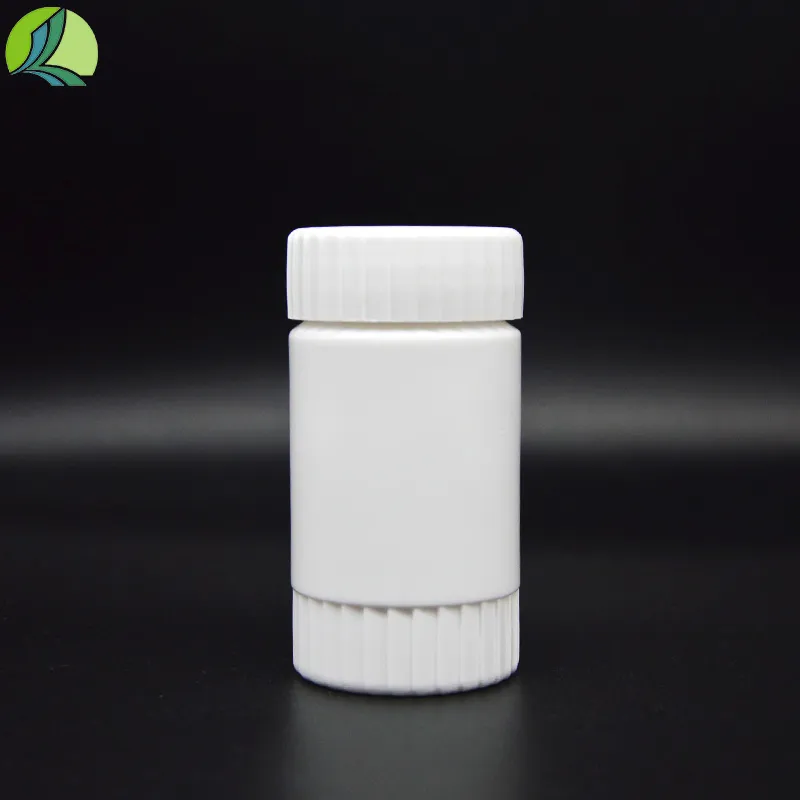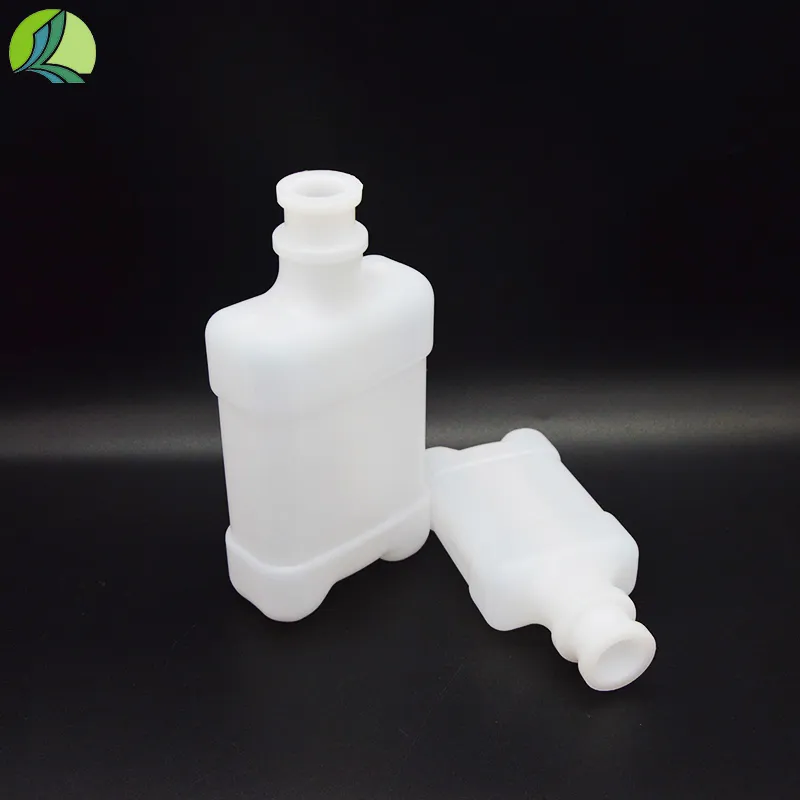
Premium Plastic Medicine Liquid Bottles & Flip Top Vials
Industry Trends and the Evolution of Pharmaceutical Packaging
The global pharmaceutical packaging market is undergoing significant transformation, driven by advancements in drug delivery systems, stringent regulatory requirements, and an increasing focus on patient safety and convenience. Central to this evolution is the demand for reliable and inert primary packaging solutions, particularly the medicine liquid bottle. Recent market analysis projects the global pharmaceutical packaging market to reach over $180 billion by 2028, with plastic container111s, including plastic drug vials and plastic medicine vials, seeing a substantial compound annual growth rate (CAGR) due to their versatility and cost-effectiveness compared to traditional glass alternatives.
Key trends influencing the design and manufacturing of modern pharmaceutical packaging include the rise of biologics and biosimilars requiring specialized barrier properties, the growing adoption of pre-filled syringes and vials for ease of administration, and an intensified scrutiny on material compatibility and extractables/leachables. Furthermore, sustainability concerns are pushing manufacturers towards recyclable or bio-based polymer solutions, while smart packaging technologies are emerging to enhance traceability and combat counterfeiting. These dynamics underscore the critical role of advanced manufacturing and material science in producing high-quality, compliant plastic drug vials for the pharmaceutical sector.
The demand for sterile vaccine vials and plastic flip top vials for medical purposes is particularly high, driven by global vaccination initiatives and the need for robust, user-friendly, and cost-effective packaging for a wide range of liquid medications.
Precision Manufacturing Process for a Sterile Medicine Liquid Bottle
The production of a high-quality medicine liquid bottle, such as the Sterile Vaccine Vial Plastic Liquid Vial For Medical Purposes, is a complex, multi-stage process that prioritizes sterility, material integrity, and dimensional precision. This ensures the chemical stability and biological safety of the contained pharmaceutical products.
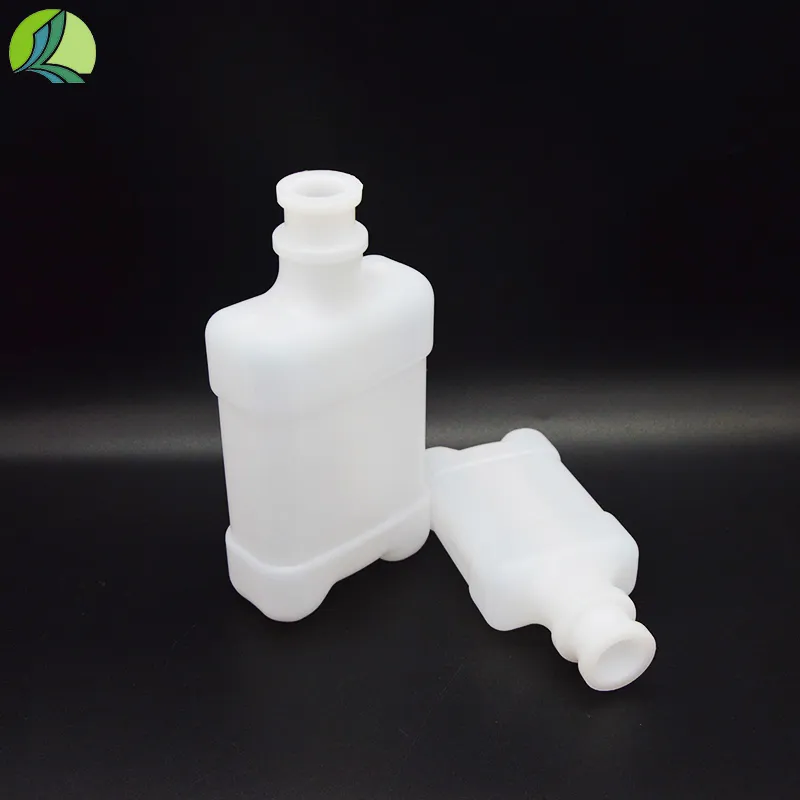
Detailed Process Flow:
- 1. Material Selection & Preparation: Utilizing medical-grade polymers such as Cyclic Olefin Copolymer (COC), Cyclic Olefin Polymer (COP), Polypropylene (PP), or High-Density Polyethylene (HDPE), which comply with USP Class VI and ISO 10993 biocompatibility standards. Raw resins undergo rigorous incoming quality control (IQC) for purity, melt flow index, and density.
- 2. Injection Molding (Preform/Body): Precision injection molding in ISO Class 7 or 8 cleanroom environments to create vial bodies or preforms. This process ensures high dimensional accuracy, uniform wall thickness, and minimizes particulate contamination. Parameters such as melt temperature, injection pressure, and cooling time are meticulously controlled using CNC machining principles applied to mold design.
- 3. Blow Molding (for Bottles): For larger plastic medicine vials, blow molding (e.g., Extrusion Blow Molding or Injection Stretch Blow Molding) forms the final bottle shape from the preform. This step is critical for achieving desired volumes, neck finishes (e.g., plastic flip top vials), and overall structural integrity.
- 4. Trimming & Finishing: Excess material is removed, and bottle openings are precisely trimmed to ensure compatibility with stoppers and caps. Automated visual inspection systems are deployed to detect defects.
- 5. Washing & Sterilization: Vials undergo a multi-stage washing process using purified water (WFI quality) to remove any residual particulate matter. Subsequent sterilization typically involves Gamma Irradiation or Ethylene Oxide (EtO) in accordance with ISO 11137 (Radiation Sterilization) or ISO 11135 (EtO Sterilization) standards, achieving a Sterility Assurance Level (SAL) of 10-6.
- 6. Particle & Dimensional Inspection: Automated inspection systems check for particulate contamination, cosmetic defects, and critical dimensional parameters (e.g., neck diameter, total height, wall thickness) to ensure compliance with specifications and global pharmacopeias (e.g., USP, EP, JP).
- 7. Packaging & Traceability: Sterilized vials are immediately packed into double or triple bagging systems within a cleanroom environment to maintain sterility. Each batch is assigned a unique identifier for full traceability from raw material to final product.
This meticulous process ensures that each medicine liquid bottle meets the highest standards for pharmaceutical use, demonstrating superior performance in target industries such as pharmaceuticals, biotechnology, diagnostics, and veterinary medicine. Advantages include enhanced energy saving through lighter weight, superior corrosion resistance to various drug formulations, and prolonged service life compared to alternative materials.
Technical Specifications: Sterile Vaccine Vial Plastic Liquid Vial
Our Sterile Vaccine Vial Plastic Liquid Vial for Medical Purposes is engineered to meet the rigorous demands of pharmaceutical and biotechnology applications. Below is a detailed specification table outlining key parameters for our flagship medicine liquid bottle.
| Parameter | Specification | Compliance/Standard |
|---|---|---|
| Product Name | Sterile Vaccine Vial Plastic Liquid Vial for Medical Purposes | Internal Ref: WK-PVL001 |
| Material | Medical-Grade Cyclic Olefin Copolymer (COC) / Polypropylene (PP) | USP Class VI, ISO 10993 Biocompatibility |
| Capacity Range | 2 mL, 5 mL, 10 mL, 20 mL, 50 mL (Customizable) | Volume Accuracy ±5% |
| Closure Type | Crimped Aluminum Cap (with stopper), Plastic Flip Top | ISO 8362 (for injectables) |
| Sterilization Method | Gamma Irradiation (Pre-sterilized) | ISO 11137, SAL 10-6 |
| Extractables/Leachables | Minimally detectable, fully compliant | USP & EP Guidelines (relevant chapters) |
| Temperature Resistance | -80°C to +121°C (Autoclavable for PP variants) | ASTM D648 |
| Barrier Properties | Excellent moisture and gas barrier (COC/COP variants) | ASTM D3985 (Oxygen), ASTM E96 (Water Vapor) |
| Transparency | High clarity (COC/COP) or translucent (PP) | ASTM D1003 (Haze) |
| Particulate Count | Conforms to USP Particulate Matter in Injections | USP |
| Regulatory Compliance | FDA 21 CFR, EU 10/2011, REACH, RoHS | Global Pharmaceutical Standards |
These specifications highlight our commitment to delivering superior plastic drug vials that ensure the safety, efficacy, and stability of critical pharmaceutical formulations.
Application Scenarios & Technical Advantages
The versatility and robust performance of our medicine liquid bottle solutions, including plastic drug vials and plastic flip top vials, enable their application across a broad spectrum of critical medical and pharmaceutical uses. Their technical advantages make them an indispensable choice for modern drug delivery.
Vaccine Packaging
Our sterile vaccine vials provide a secure and inert primary container111 for sensitive vaccine formulations. Their robust polymer construction minimizes the risk of breakage during transport and storage, a critical advantage over traditional glass vials, especially in mass vaccination campaigns. The material's low protein adsorption ensures the integrity and efficacy of biological products.
Sterile Injectable Drugs
For parenteral drugs, our plastic medicine vials offer superior protection against delamination and particle shedding, common issues with glass. Pre-sterilized options eliminate the need for in-house sterilization, streamlining aseptic filling processes and reducing the risk of contamination in sterile environments.
Ophthalmic & Nasal Solutions
The precision-engineered neck finishes on our plastic drug vials are ideal for dispensing ophthalmic and nasal solutions, ensuring accurate drop control and preventing leakage. The inert nature of the polymer protects sensitive formulations from chemical interaction, maintaining product stability.
Diagnostic Reagents & Kits
In diagnostic applications, the chemical resistance of our plastic vials is paramount. They safely house various reagents without affecting their sensitivity or reactivity, supporting reliable and accurate diagnostic testing across medical laboratories.
Key Technical Advantages:
- Enhanced Safety & Breakage Resistance: Eliminates glass breakage risks, crucial for patient safety and reducing product loss during logistics and administration. This is particularly vital for plastic drug vials.
- Reduced Extractables & Leachables: Medical-grade polymers are selected for their minimal interaction with drug formulations, preserving drug purity and stability, a critical factor for any medicine liquid bottle.
- Lightweight & Cost-Effective Logistics: Significant reduction in weight compared to glass, leading to lower shipping costs and carbon footprint, aligning with sustainable practices.
- Design Flexibility: Allows for diverse shapes, sizes, and closure types, including the highly convenient plastic flip top vials, catering to specific drug delivery needs and branding.
- Gamma & Autoclavable Sterilization Compatibility: Suitable for standard sterilization methods without material degradation, ensuring terminal sterility for critical applications.
- Dimensional Stability: Precision manufacturing ensures consistent dimensions for automated filling and capping lines, minimizing operational inefficiencies.
Vendor Comparison: Selecting the Optimal Medicine Liquid Bottle Supplier
Choosing the right supplier for a medicine liquid bottle is paramount for pharmaceutical companies, as it directly impacts drug integrity, regulatory compliance, and supply chain reliability. A thorough vendor comparison goes beyond mere pricing to evaluate critical aspects of quality, innovation, and service.
| Criterion | Leading Industry Standard (e.g., WKPacking) | Typical Industry Vendor |
|---|---|---|
| Material Quality & Certifications | USP Class VI, ISO 10993, FDA DMF support, rigorous IQC. Dedicated cleanroom polymer handling. | General medical-grade polymers, fewer specific drug master file (DMF) references. |
| Manufacturing Environment | ISO Class 7/8 Cleanrooms for molding, filling, and final packaging. | Controlled environments, but not always ISO-certified cleanrooms for all stages. |
| Sterilization Assurance | Validated Gamma Irradiation (SAL 10-6) with documented certificates. | May offer non-sterile or less stringently validated sterilization. |
| Customization Capabilities | Extensive design, material, color, and closure customization (e.g., plastic flip top vials) with R&D support. | Limited to standard molds and basic color options. |
| Quality Control & Inspection | Automated optical inspection, CMM, extractables/leachables testing, particulate analysis (USP & EP). | Manual/sampled inspection, less comprehensive analytical testing. |
| Technical Support & Expertise | Dedicated technical team, regulatory affairs support, long-term stability data. | Basic sales support, limited post-delivery technical assistance. |
| Lead Time & Supply Chain Reliability | Optimized production lines, strategic inventory, global logistics partnerships for consistent supply. | Variable lead times, potential for supply chain disruptions due to limited capacity. |
Companies adhering to leading industry standards, exemplified by our operations, demonstrate a profound commitment to quality, regulatory compliance, and client partnership. This ensures that every plastic drug vial and medicine liquid bottle delivered meets the highest pharmaceutical standards.
Customized Solutions for Plastic Medicine Vials
Recognizing that standard solutions do not always meet the unique requirements of every pharmaceutical product, we offer extensive customized solutions for our medicine liquid bottle range, including specialized plastic drug vials and plastic flip top vials. Our engineering team collaborates closely with clients to develop bespoke primary packaging that perfectly aligns with their drug formulation, administration route, and branding strategy.
- Material Customization: Selection of specific polymers (e.g., COC, COP, PP, HDPE, PET) based on drug compatibility, barrier requirements, temperature stability, and optical clarity needs. This includes advising on grades optimized for low extractables or enhanced UV protection.
- Design & Dimension Modifications: Tailored vial dimensions (height, diameter, neck finish), specific fill volumes, and unique aesthetic designs. This encompasses specialized neck designs for precise dispensing or child-resistant closures.
- Barrier Property Enhancement: Incorporation of advanced barrier technologies for formulations sensitive to oxygen, moisture, or light, extending product shelf-life and stability.
- Color & Opaque Options: Custom color matching for brand consistency or opaque vials for light-sensitive drugs, with options for UV-blocking additives.
- Integrated Features: Development of vials with integrated dosage cups, special tamper-evident features, or components for specific drug delivery devices.
- Surface Treatment & Coatings: Application of internal coatings (e.g., siliconization) to reduce drug adsorption or improve fill-finish line efficiency.
- Assembly & Kitting: Providing ready-to-use solutions by assembling plastic medicine vials with stoppers, caps, or other components, and kitting them for streamlined operations.
Our comprehensive customization process ensures that the final medicine liquid bottle is not just a container111, but an integral part of your product's success.
Application Case Studies: Real-World Impact of Our Plastic Drug Vials
Our commitment to delivering high-performance medicine liquid bottle solutions is validated by successful collaborations with leading pharmaceutical companies worldwide. These case studies demonstrate how our plastic drug vials and plastic medicine vials provide tangible benefits in real-world scenarios.
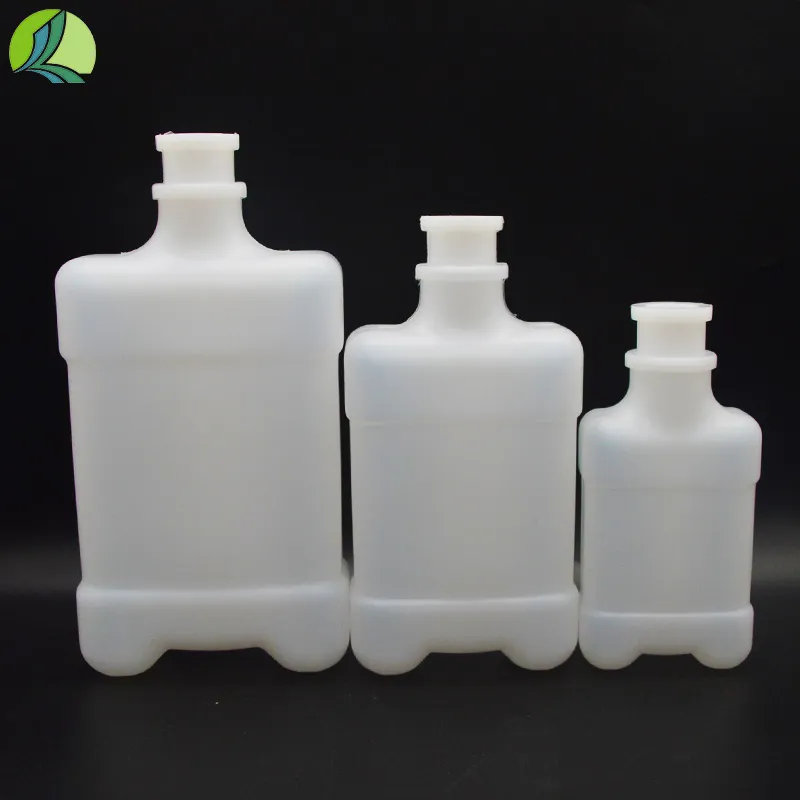
Case Study 1: Global Vaccine Distribution
A leading global pharmaceutical firm needed a robust, lightweight, and sterile primary packaging solution for a newly approved vaccine targeted for mass distribution in developing regions. Traditional glass vials posed significant challenges due to fragility, weight, and high transport costs.
Solution: We provided custom-designed 10mL plastic vaccine vials made from medical-grade COC, pre-sterilized via Gamma Irradiation. The vials featured enhanced barrier properties and a secure crimp finish compatible with existing filling lines.
Outcome: The client reported a 70% reduction in in-transit breakage, a 25% decrease in shipping costs due to lighter weight, and significantly improved cold chain integrity. The switch to our medicine liquid bottle enabled faster, safer, and more economical vaccine distribution to critical populations.
Case Study 2: Biologic Drug Stability Enhancement
A biotechnology company developing a sensitive monoclonal antibody formulation faced challenges with protein adsorption and aggregation when stored in conventional glass vials, impacting drug efficacy and shelf life.
Solution: We collaborated to develop a bespoke 5mL plastic medicine vial using a specially formulated, low-protein-adsorbing polymer. The vials underwent a unique surface treatment process and were rigorously tested for extractables and leachables.
Outcome: Long-term stability studies confirmed a significant reduction in protein adsorption and aggregation, extending the drug's shelf life by 6 months. This critical improvement enabled the client to secure market approval and expand their therapeutic reach.
Case Study 3: Over-the-Counter Pediatric Medication
A consumer healthcare company needed a child-friendly, easy-to-use primary package for a new line of pediatric liquid medications. The design needed to be robust, offer a convenient dispensing mechanism, and appeal to parents.
Solution: We engineered a custom 30mL plastic flip top vial made from pharmaceutical-grade HDPE, featuring an integrated, tamper-evident cap and a precise orifice for controlled dosing. The design incorporated vibrant, child-safe colors and a smooth, ergonomic shape.
Outcome: The new plastic drug vials were highly successful in market, receiving positive feedback for ease of use and safety. The robust design minimized leakage and breakage complaints, solidifying the brand's reputation for quality and innovation.
Frequently Asked Questions (FAQ)
Q1: What materials are your medicine liquid bottle products made from?
A1: Our plastic drug vials are primarily manufactured from medical-grade Cyclic Olefin Copolymer (COC), Cyclic Olefin Polymer (COP), Polypropylene (PP), and High-Density Polyethylene (HDPE). All materials comply with USP Class VI and ISO 10993 biocompatibility standards.
Q2: What sterilization methods do you use for plastic medicine vials?
A2: Our sterile vaccine vials are typically pre-sterilized using Gamma Irradiation, adhering to ISO 11137 standards and achieving a Sterility Assurance Level (SAL) of 10-6. We also offer options for Ethylene Oxide (EtO) sterilization based on specific client requirements.
Q3: Can these plastic flip top vials be customized for specific drug formulations?
A3: Yes, we offer extensive customization options, including material selection, specific dimensions, barrier property enhancements, color matching, and integration of unique features. Our R&D team works closely with clients to ensure optimal drug compatibility and packaging performance.
Q4: What are your minimum order quantities (MOQ)?
A4: MOQs vary depending on the specific product and level of customization. Please contact our sales team with your specific requirements for a detailed quotation and MOQ information.
Q5: Do your products comply with international regulatory standards?
A5: Absolutely. All our medicine liquid bottle products are manufactured in compliance with stringent international standards including FDA 21 CFR, EU 10/2011, REACH, RoHS, and relevant pharmacopeias (USP, EP, JP). We provide full documentation and support for regulatory submissions.
Lead Time, Warranty, and After-Sales Support
We understand the critical importance of reliable supply chains and robust support for pharmaceutical packaging. Our operational framework for the medicine liquid bottle is designed to provide seamless service from order to post-delivery.
Lead Time & Fulfillment
- Standard Products: Typical lead times for standard plastic drug vials range from 4 to 6 weeks, depending on volume and current production schedules.
- Customized Solutions: Lead times for custom plastic medicine vials or plastic flip top vials will be mutually agreed upon during the project development phase, typically ranging from 8 to 14 weeks, inclusive of mold development and sample validation.
- Logistics: We leverage a global network of logistics partners to ensure timely and secure delivery worldwide, offering various shipping options including expedited services where needed.
Warranty Commitments
We stand behind the quality and performance of our products. All our medicine liquid bottle products are covered by a comprehensive warranty against manufacturing defects and material non-compliance for 12 months from the date of shipment. This warranty ensures that our plastic drug vials meet all agreed-upon technical specifications and regulatory standards. Detailed warranty terms are available upon request.
Customer Support & After-Sales Service
- Dedicated Account Management: Each client is assigned a dedicated account manager to ensure clear communication and personalized service throughout the partnership.
- Technical Support: Our team of packaging engineers and material science experts is available to provide technical assistance, troubleshooting, and support for product integration into your filling lines.
- Quality Assurance: We maintain a robust quality assurance system and provide full traceability for all products. In the unlikely event of a quality concern, our QA team will promptly investigate and implement corrective actions.
- Regulatory Documentation: We provide comprehensive documentation packages to support your regulatory submissions, including material certifications, extractables/leachables data, and sterilization certificates.
Conclusion
The selection of a high-quality medicine liquid bottle is a critical decision that impacts drug safety, efficacy, and ultimately, patient well-being. Our sterile vaccine vials and plastic medicine vials represent the pinnacle of pharmaceutical packaging innovation, combining advanced material science with precision manufacturing. By adhering to the highest regulatory standards and offering extensive customization, we empower pharmaceutical companies to deliver their life-saving medications with unparalleled confidence and efficiency. Our commitment to expertise, experience, authoritativeness, and trustworthiness ensures that every plastic drug vial we produce contributes to a safer and more effective global healthcare system.
References
- United States Pharmacopeia. USP 43–NF 38. Rockville, MD: United States Pharmacopeial Convention; 2020.
- European Directorate for the Quality of Medicines & HealthCare (EDQM). European Pharmacopoeia 10th Edition. Council of Europe; 2020.
- ISO 11137-1:2006, Sterilization of health care products — Radiation — Part 1: Requirements for development, validation and routine control of a sterilization process for medical devices.
- ISO 10993-1:2018, Biological evaluation of medical devices — Part 1: Evaluation and testing within a risk management process.
- FDA 21 CFR Part 210, Current Good Manufacturing Practice in Manufacturing, Processing, Packing, or Holding of Drugs; General.
-
Bulk Eye Dropper Bottles for Industrial Packaging - Reliable & CustomizableNewsDec.31,2025
-
Small Plastic Dropper Bottles – Durable, Precise Packaging Solutions for B2B ApplicationsNewsDec.10,2025
-
Medicine Dropper Bottles – Precision and Quality Packaging Solutions for B2B | WK PackingNewsDec.10,2025
-
Discover Top Quality 2 oz Eye Dropper Bottles for Industrial UseNewsDec.09,2025
-
1 Oz Eye Dropper Bottles - Precision Packaging Solutions for B2B Industries | WKPackingNewsDec.09,2025
-
Durable 4 oz Eye Dropper Bottles for Industrial & Cosmetic UseNewsDec.09,2025